Layer Battery Cage Selection: Matching Capacity, Wire Design and Farm Layout
Key Takeaways
- When does cross border manufacturing expansion reduce total landed cost?IT & Security Director
- How technological forecasting helps manufacturers time automation investmentsChief Civil Engineer
- How food traceability solutions help contain recall risks fasterAgri-Tech Strategist
- What low-light performance should an OEM night vision dash cam meet?Automotive Tech Analyst
- Adipic Acid CAS 124-04-9 Market Trends: Why Buyers Are Rebuilding Supply PlansLead Materials Scientist
- Titanium Dioxide Dispersion: Key Factors for Coating Opacity and StabilityLead Materials Scientist
- Reducing Operational Carbon: Applying LEED v4.1 Emissions RequirementsIT & Security Director
- LEED v4.1 Emissions Primer: What Project Teams Must Document for ComplianceChief Civil Engineer
Industry Overview
We do not just publish news; we construct a high-fidelity digital footprint for our partners. By aligning with TNE, enterprises build the essential algorithmic "Trust Signals" required by modern search engines, ensuring they stand out to high-net-worth buyers in an increasingly crowded global digital landscape.
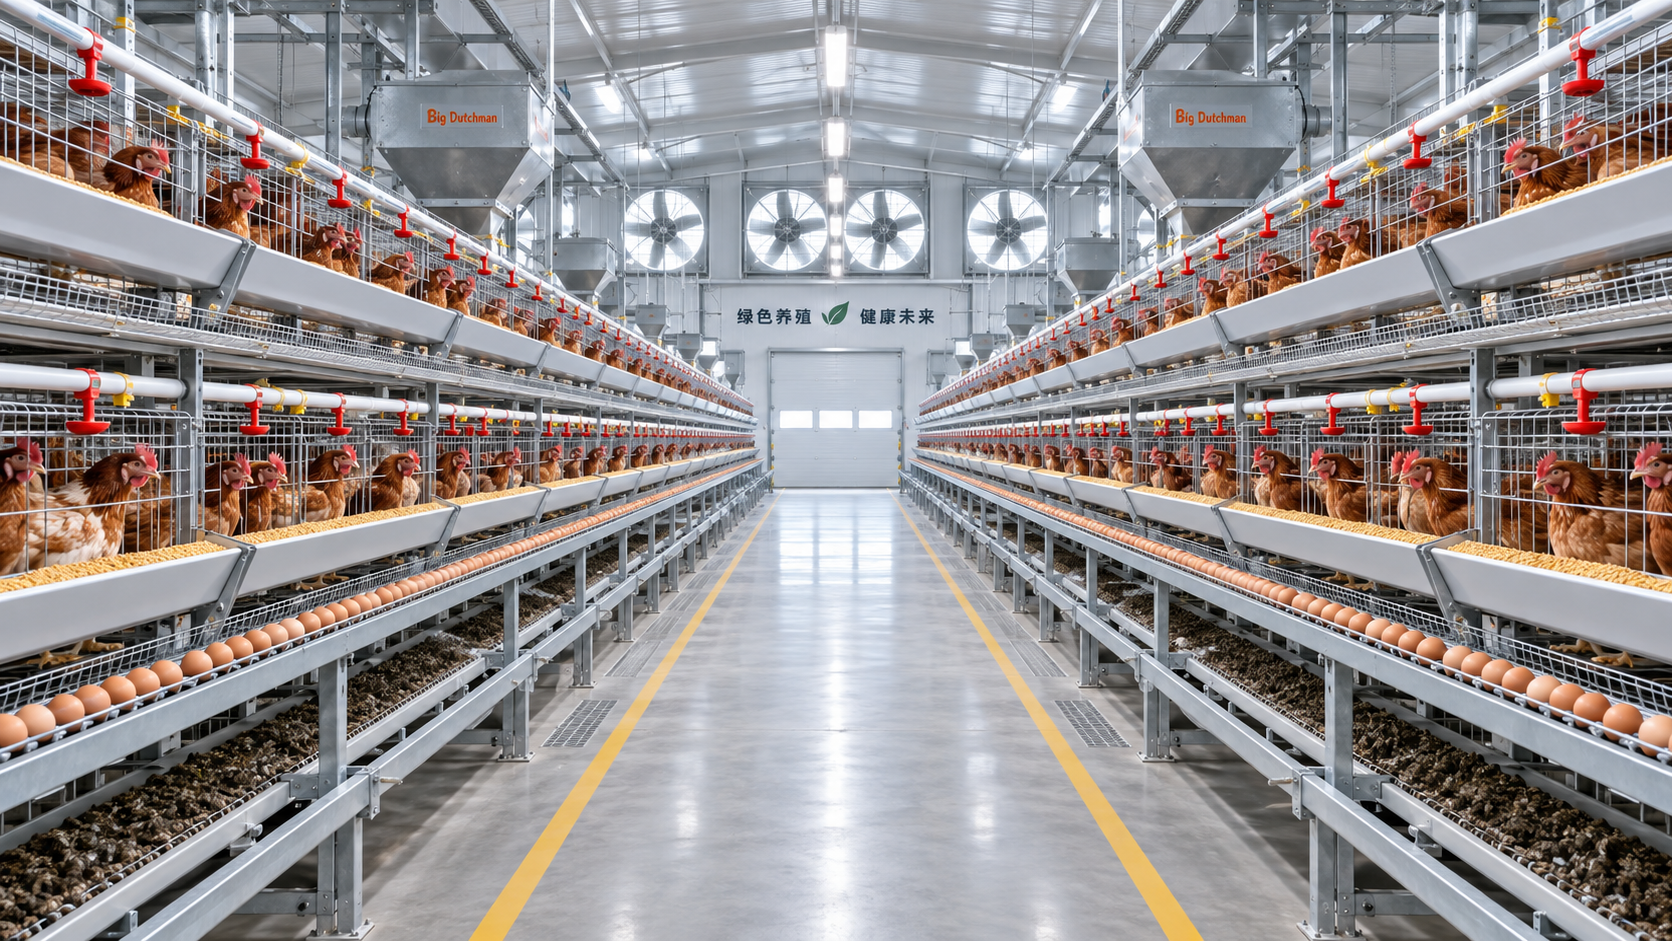
A layer cage system should be selected from the inside out: begin with the flock size and production target, then test whether cage geometry, wire construction, manure handling, ventilation, and building circulation can support that target. A system that appears economical on a per-cage basis can create persistent operating problems if bird density, feeder access, egg collection routes, or service aisles are mismatched to the farm layout.
For technical evaluation teams, the central question is not simply how many birds a house can hold. It is whether the proposed capacity can be managed consistently through the laying cycle without creating avoidable stress on birds, staff, equipment, or the building itself. Capacity planning, wire specification, and layout design should therefore be reviewed as one engineering decision rather than separate purchasing items.
Start With Usable Capacity, Not Nominal Cage Count
Suppliers may describe a system by the number of tiers, cells, rows, or birds per unit. These figures are useful for comparison, but they do not by themselves establish usable farm capacity. The practical number of layers depends on the internal cage dimensions, number of birds assigned to each compartment, feeder and drinker arrangement, ventilation distribution, local welfare requirements, and the farm’s ability to monitor and maintain the system.
A higher bird count per cage compartment can reduce the initial structural cost per bird, but it can also narrow the margin for operational variation. Differences in flock uniformity, heat load, pecking behavior, water availability, and feeder performance become more consequential when birds have less effective access to resources. In a well-managed house with stable environmental control, a denser layout may be workable. In a house subject to high ambient temperatures, uneven air movement, frequent manual intervention, or variable flock quality, additional space and easier access often provide a more forgiving operating condition.
Technical teams should distinguish between installed capacity and operational capacity. Installed capacity is the maximum number of birds indicated by the cage arrangement. Operational capacity is the number that can be housed while maintaining routine inspection, collection, feeding, drinking, manure removal, and mortality handling without congestion. The second figure is usually more useful for budgeting labor, utility demand, replacement parts, and expected workflow.
Questions that clarify capacity assumptions
- How many birds will occupy each cage compartment at the intended production stage?
- What usable floor area, feeder length, and drinker access are available per bird?
- Can staff inspect birds in upper and lower tiers without unsafe reaching or restricted sightlines?
- Will egg collection, manure removal, and feeding equipment operate at the planned stocking level without obstructing one another?
- Does the ventilation design account for the heat and moisture load associated with the actual flock size?
These questions are especially important when a farm expands an existing building. Increasing the number of tiers or extending rows may change the building’s internal heat balance, electrical loading, service access, and evacuation routes. A cage system should fit the house as a working environment, not merely occupy its available floor area.
Wire Design Determines More Than Structural Appearance
Wire mesh is often evaluated visually during procurement, yet its design affects egg handling, bird support, cleaning, corrosion exposure, and long-term structural stability. A cage can look rigid when empty but behave differently after birds, feeders, drinker lines, manure accumulation, and repeated maintenance loads are introduced.
Evaluation should begin with the relationship between wire diameter, mesh opening, welding quality, surface treatment, and supporting frame arrangement. Thicker wire may improve resistance to deformation, but diameter alone is not a complete quality indicator. Wire spacing influences foot support and manure passage; weld consistency affects resistance to loosening; and the protective coating must be suitable for a humid, ammonia-exposed poultry environment.
The cage floor requires particularly close review. It must provide stable footing while allowing eggs to roll toward the collection area in a controlled manner. If the slope, mesh geometry, or front-edge arrangement is poorly matched, eggs may stop before reaching the collection zone, collide with other eggs, or become more exposed to dirt and breakage. Floor deformation can worsen these issues over time, especially where support points are too widely spaced or where the cage is loaded beyond its intended design condition.
Sharp edges, inconsistent cut-wire finishing, damaged galvanizing, and weak weld joints should be treated as inspection issues rather than cosmetic defects. Such details may create injury points, rust initiation sites, or areas that collect debris. During a pre-shipment or site acceptance inspection, teams can examine representative cage panels rather than relying only on a single display sample. Checks should include panel flatness, consistency of mesh openings, weld continuity, coating coverage around joints, and alignment after assembly.
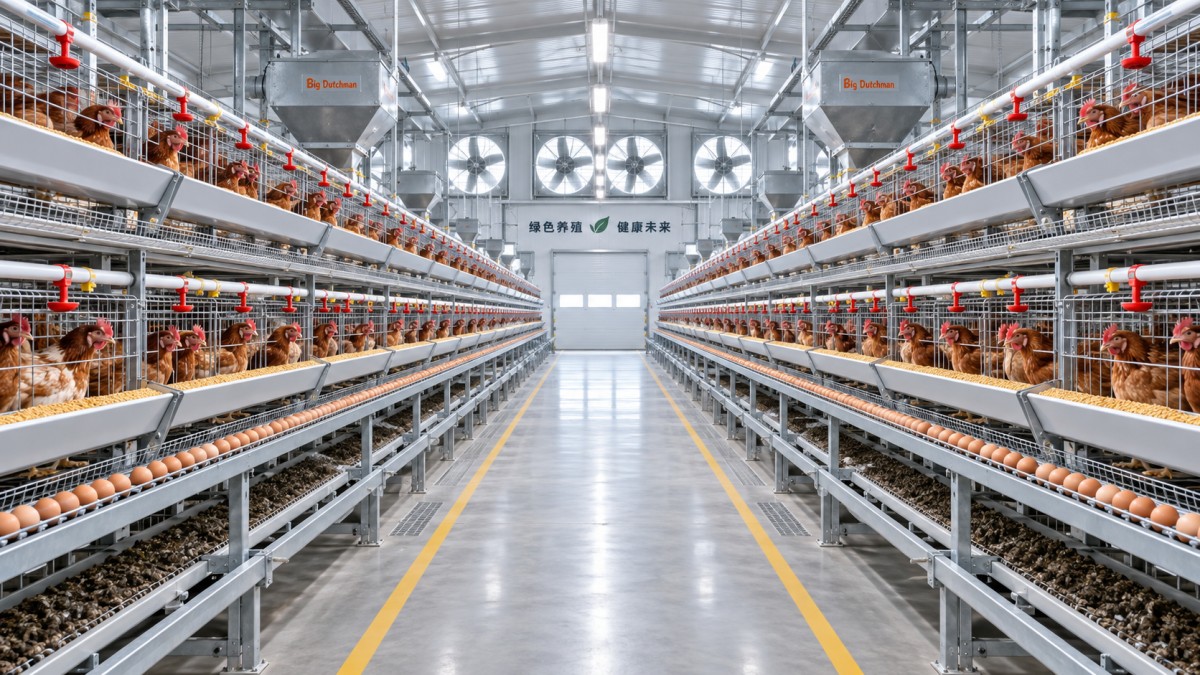
Match the Cage Configuration to the Building Envelope
Farm layout decisions often fail when cage rows are designed independently from the building. A technically sound cage line can still be difficult to operate if it leaves inadequate room for service aisles, egg collection equipment, electrical panels, water filtration units, manure discharge points, or ventilation inlets.
Before selecting a tier configuration, create a scaled layout that includes the full building length and width, column locations, door clearances, drainage points, wall openings, roof height, and equipment rooms. The drawing should show more than cages. It should also include walkways, cross aisles, end-of-row access, feed transport paths, egg handling areas, and the route used to remove manure from the house.
Tier height must be evaluated against the building’s clear internal height and the need for maintenance access above the top tier. In houses with limited roof clearance, the upper tier may be positioned too close to hot air accumulation zones or become difficult to inspect. Where mechanical ventilation is used, the placement of inlets, fans, baffles, and cage rows should be coordinated so that air reaches all levels with reasonable uniformity. Airflow that bypasses lower tiers or stagnates around end sections can create uneven production conditions even when the cage equipment itself is correctly installed.
Equipment Interfaces Often Decide Day-to-Day Reliability
A layer cage is part of a system rather than a standalone steel structure. The selection process should examine its interfaces with feed delivery, nipple drinkers, egg collection, manure belts or scrapers, lighting, and control equipment. Many operational issues originate where these systems meet.
For example, drinker lines must be positioned so birds can reach them without creating persistent wet areas beneath the nipples. Water pressure regulation, line flushing arrangements, and access to filters should be considered before cages are installed. A small leak can affect cage hygiene, manure condition, and corrosion exposure over a long period, particularly in multi-tier arrangements where water may travel downward.
Feed trough design and mounting position should also be assessed in relation to bird access and cleaning. A trough that is difficult to inspect may allow feed accumulation, contamination, or uneven distribution to go unnoticed. If automated feed equipment is included, maintenance access to drive units, corners, and tensioning components needs to be available without dismantling cage sections.
Egg collection systems require alignment across cage rows. Tracks, belts, rollers, and transfer points need a stable mounting arrangement, because minor level differences can contribute to egg congestion or damage. The farm should also determine how eggs will move from the house to grading, packing, or temporary storage. A well-designed collection belt does not eliminate the need for adequate room at the transfer end of the building.
When reviewing a layer cage page such as Taiyu(HK) poultry farm equipment, an evaluator can use the listed configuration as a reference point for checking how a Type 1 layer cage arrangement may relate to the farm’s intended bird capacity, row spacing, and supporting equipment. The useful assessment is not whether one layout fits every farm, but whether the available structure and system interfaces can be adapted to the building and operating plan under review.
Material Protection Should Be Judged by the House Environment
Corrosion is rarely caused by a single factor. It develops through the combined effect of moisture, manure gases, dust, cleaning practices, water leakage, coating damage, and the time that surfaces remain wet. Cage material selection should reflect the expected environment rather than relying on a general statement that a finish is corrosion resistant.
Technical specifications can request clarity on the base material, coating method, coating condition at welded areas, and the treatment of fasteners, brackets, and support members. Components near drinker lines, manure zones, wash-down areas, and building openings may face different exposure conditions from protected central sections. If replacement of corroded parts would require disassembly of adjacent cage rows, the accessibility of those components deserves extra attention.
Cleaning method also matters. Aggressive washing, poorly controlled chemicals, and insufficient drying can shorten the service life of metal components. The farm’s maintenance plan should identify what can be cleaned in place, where residue may gather, and how damaged coatings will be monitored. This is a practical consideration for both new construction and retrofit projects, where old building moisture problems may persist after new cages are installed.
Procurement Documents Should Convert Assumptions Into Verifiable Requirements
A technical procurement file should describe the required outcome, not just list the number of cages. It can include the proposed house dimensions, tier arrangement, intended bird allocation, major equipment interfaces, material expectations, delivery condition, installation scope, spare-part assumptions, and acceptance checks. This approach helps prevent a quotation from being compared only on total price or nominal capacity.
For a multi-supplier comparison, request drawings that show row spacing, cage dimensions, feed and water position, egg collection route, manure handling arrangement, and support points. Ask whether the system is supplied knocked down or pre-assembled, since packaging method affects installation sequence, inspection effort, and the likelihood of parts being misplaced on site. Where installation is performed by the farm or a local contractor, clear component identification and assembly instructions become operational risk controls rather than administrative extras.
Acceptance inspection should occur before birds are introduced. Check structural alignment, anchoring, moving equipment operation, drinker line integrity, feeder movement, electrical protection, belt tracking where applicable, and clearance around access points. Running each subsystem under no-load conditions is useful, but the commissioning plan should also account for how equipment will be observed after flock placement, when vibration, heat, moisture, and daily operating cycles begin to reveal hidden alignment issues.
A Selection Decision That Remains Usable After Installation
The strongest layer cage selection is one that remains manageable when routine conditions are less than perfect: a worker needs to inspect a lower row, a drinker line requires flushing, a belt needs adjustment, a fan is serviced, or a section must be cleaned while the house continues operating. Capacity matters, but capacity without access and environmental control can transfer cost from construction to daily labor and maintenance.
Technical evaluators should treat the cage as part of an integrated farm layout. Review bird allocation alongside usable floor area, examine wire design alongside corrosion exposure and egg handling, and test the planned row arrangement against ventilation, manure removal, and service access. A system chosen on those combined conditions is more likely to support consistent farm use than one selected from a capacity figure alone.
Deep Dive
Related Intelligence
 Smart Livestock & Poultry TechHow poultry housing systems improve flock health and reduce labor costs in commercial farmsAnalyst:Agri-Tech Strategist
 Smart Livestock & Poultry TechWhat livestock management features matter most when scaling a multi-site poultry operation in 2026Analyst:Agri-Tech Strategist
 Smart Livestock & Poultry TechCan automated farming solutions integrate with existing ventilation and feeding hardware on legacy poultry farmsAnalyst:Agri-Tech Strategist