When does procurement research in the USA justify a local supplier audit?
Key Takeaways
- When does procurement research in the USA justify a local supplier audit?IT & Security Director
- How chemical applications in coatings improve corrosion resistanceLead Materials Scientist
- How to size small scale grain milling equipment for daily outputAgri-Tech Strategist
- How specialty chemical research reduces scale-up riskLead Materials Scientist
- When does industrial IoT for factories reduce unplanned downtime?Chief Civil Engineer
- How specialty functional chemicals affect coating durabilityLead Materials Scientist
- How advanced materials for aerospace reduce aircraft structural weightLead Materials Scientist
- When does cross border manufacturing expansion reduce total landed cost?IT & Security Director
Industry Overview
We do not just publish news; we construct a high-fidelity digital footprint for our partners. By aligning with TNE, enterprises build the essential algorithmic "Trust Signals" required by modern search engines, ensuring they stand out to high-net-worth buyers in an increasingly crowded global digital landscape.
Local supplier audits in the United States are justified when a sourcing decision carries consequences that supplier questionnaires, pricing sheets, certificates, and video calls cannot reliably resolve. The practical threshold is simple: arrange an on-site assessment when a failure in quality, delivery, traceability, security, or continuity would cost more than the visit and the corrective work it may trigger.
Desk-based procurement research USA is valuable for narrowing a field. It can compare product ranges, public records, quoted lead times, freight lanes, financial signals, technical documentation, and stated quality systems. It cannot show whether the quoted process is actually used on the relevant production line, whether capacity is protected during peak demand, or whether a critical subcontractor controls a step that was presented as in-house.
An audit should therefore be treated as a decision tool, not a ceremonial approval step. The purpose is to test the assumptions that materially affect total landed cost and operational exposure.
Start with the cost of being wrong
A local audit becomes easier to justify when the purchase has a high cost of failure. That cost is not limited to the unit price of defective goods. It can include incoming inspection, production stoppage, rework, expedited freight, field replacement, inventory write-offs, delayed installation, missed customer commitments, and engineering time spent isolating the cause.
A low-value catalog item with multiple approved alternatives rarely needs the same level of scrutiny as a custom-molded component, a food-contact material, a structural assembly, a software-enabled control device, or a chemical input that affects downstream processing. The distinction is not simply whether an item is expensive. A modestly priced gasket, fastener, resin additive, sensor, or network appliance can create disproportionate disruption when it is difficult to substitute or when its failure appears only after assembly.
Consider a quoted part that meets a drawing dimension but requires a specific surface finish, cure profile, fiber orientation, heat treatment, or firmware version. Research may confirm that the supplier has relevant equipment. It does not establish that the equipment is maintained, that the process window is controlled, or that inspection results are linked to individual lots. A site visit is warranted when these hidden conditions determine whether the part functions as intended.
Signals that desk research has reached its limit
Contradictions between sources are one of the clearest triggers. A supplier may describe a facility as vertically integrated while its documentation refers vaguely to “production partners.” A capacity statement may exceed what the visible equipment footprint, staffing pattern, or stated operating schedule appears able to support. A quote may promise short lead times while raw-material lead times or finishing steps suggest otherwise. None of these observations proves poor performance, but each identifies an assumption that deserves direct examination.
Unusual price positioning requires the same discipline. A price that is materially below comparable offers can reflect efficient automation, lower overhead, a different material grade, omitted testing, thinner packaging, outsourced labor, or an incomplete understanding of the specification. Price alone does not reveal which explanation applies. The audit should trace the quoted cost through the actual route: incoming material, fabrication, inspection, packaging, storage, and dispatch. This is especially important where an apparently minor process omission could transfer cost downstream.
New suppliers also deserve closer attention when the purchase is technically or operationally sensitive. A polished website, a complete capability statement, and responsive commercial communication are useful signals, but they are not evidence that the proposed product has been manufactured repeatedly under stable conditions. The relevant question is whether the site has handled comparable material behavior, tolerances, volumes, packaging requirements, and change-control expectations.
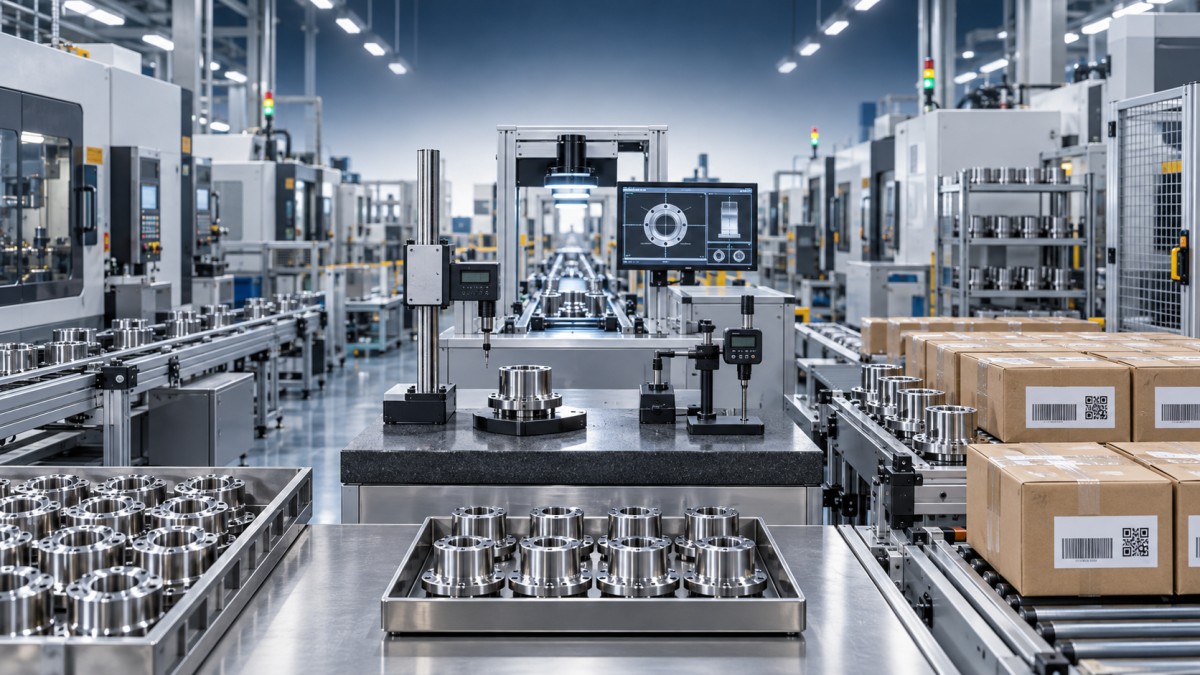
Audits are also justified when a supplier is changing something fundamental: relocating production, adding a second shift, bringing a process in-house, switching a key raw material, replacing enterprise software, or expanding into a new product category. Historical performance may not transfer cleanly through these changes. A visit can establish whether work instructions, equipment qualification, inspection planning, and inventory controls have moved with the operation.
Capacity claims need physical context
Capacity is frequently misunderstood because a monthly output figure says little about usable capacity for a specific order. A facility can possess sufficient machines yet still be constrained by tooling changeovers, curing ovens, test stations, skilled setup labor, clean-room access, programming resources, material staging, or a single outsourced operation. The bottleneck is often outside the machine that appears central to the product.
During an audit, the production route should be followed in the same order as the proposed item. For fabricated metalwork, that may mean examining material receipt, cutting, forming, welding, machining, coating, final inspection, and packing. For an electronics assembly, the critical path may run through component storage, programmed placement, soldering, inspection, functional test, firmware loading, and configuration control. For engineered polymers, drying conditions, moisture management, mold maintenance, regrind practices, and cooling time may matter more than the press count.
Visible idle equipment should not automatically be read as spare capacity. It may be awaiting maintenance, reserved for another program, unsuitable for the required tolerance, or missing qualified tooling. Conversely, a compact facility can be reliable when it has disciplined scheduling, stable external processing, and clear control of the limiting operation. The audit should distinguish between installed capacity, demonstrated throughput, and capacity genuinely available during the expected demand window.
Quality evidence is strongest when it connects to the floor
Audit effort should focus on the quality controls that prevent the defect most likely to cause harm, rather than collecting every available document. For a machined component, the relevant evidence may be how tool wear is recognized, how measurement devices are controlled, and how a nonconforming batch is separated from accepted stock. For coated construction materials, the important issue may be surface preparation, environmental conditions during application, cure verification, and handling before installation. For food-system equipment, cleanability, material segregation, sanitation access, and lot identification may be central.
Inspection equipment by itself is weak evidence. A coordinate measuring machine, hardness tester, environmental chamber, or functional test rack may be present but not included in normal release activity. Ask to see a recent record tied to a real production lot, then trace that lot through incoming material, work order, inspection result, packaging label, and shipment record. Gaps in this chain are more informative than a perfectly organized document folder.
Traceability deserves particular attention where substitutions are difficult or where a problem could surface after installation. Batch codes need to remain meaningful after cutting, blending, kitting, relabeling, or repacking. A supplier may accurately retain a raw-material certificate yet lose the link between that material and the finished shipment. The practical test is whether a specific delivered unit could be connected to its inputs, processing record, inspection status, and any deviation approval without reconstructing the story from memory.
Subcontracting changes the audit scope
Many capable U.S. suppliers depend on external services for plating, heat treatment, sterilization, calibration, die casting, cable harness work, cloud hosting, warehousing, or specialty testing. Outsourcing is not a defect. It becomes a concern when the external step is critical to fit, performance, regulatory obligations, confidentiality, or delivery timing and is not clearly disclosed.
A local audit should establish where ownership of control changes. Does the supplier qualify the subcontractor against the same specification? Are incoming checks performed after the work returns? Can a deviation be identified before it reaches final assembly? Is there an alternate source, and would switching it require new validation? A supplier that manages a controlled external process transparently can be lower risk than one claiming broad capabilities while leaving accountability unclear.
The same logic applies to digital products and connected equipment. A local visit may be justified when software configuration, secure provisioning, repair access, source-code custody, or incident response affects the delivered solution. A demonstration environment can be polished while production release procedures, access permissions, backup restoration, and vulnerability handling remain untested. The audit should examine the controls attached to the actual release path, not only the functionality shown in a meeting.
When logistics and site conditions make a visit worthwhile
Local sourcing is often assumed to reduce supply risk, but the final miles of the chain still matter. An audit can reveal whether finished goods are stored indoors, whether moisture-sensitive materials are sealed correctly, whether mixed orders are labeled distinctly, and whether loading practices protect surfaces, edges, electronics, or temperature-sensitive goods. These details affect delivered quality even when manufacturing is sound.
For large fabricated assemblies or installation-dependent products, the audit should include packaging and dispatch readiness. A structural panel, charging enclosure, industrial cabinet, or process skid may meet the fabrication drawing yet arrive with lifting points that do not match the installation plan, insufficient protection for transit vibration, or incomplete field documentation. These failures are expensive because they emerge after labor, site access, and equipment have already been scheduled.
Facility location also affects recovery options. A supplier near a major customer site may still rely on a distant finishing house, a congested freight terminal, or a single material distributor. The point is not to reject such arrangements automatically. It is to understand the elapsed time between detecting a defect and producing a corrected replacement, including engineering review, material replenishment, rework, testing, packing, and transport.
Use a proportionate audit rather than a generic tour
The audit depth should follow the uncertainty that triggered it. A short pre-award visit may be enough when the question is whether the proposed work is genuinely performed at the stated site. A more detailed technical audit is appropriate when approval depends on process capability, special handling, traceability, or supplier-managed design changes.
- For a straightforward repeat purchase, concentrate on the quoted production route, release records, storage conditions, and the visible source of any critical external work.
- For custom or engineered items, review the path from drawing revision to work instruction, tooling or programming control, first-piece approval, measurement method, and disposition of rejected material.
- When continuity is the concern, examine capacity commitments alongside cross-training, preventive maintenance, material availability, backup equipment, and how production priorities are changed when a disruption occurs.
- Where the product enters a sensitive environment, include packaging integrity, cleaning controls, configuration management, chain of custody, or secure handling according to the failure mode that matters after delivery.
The visit should end with evidence, not impressions. Record the specific process observed, the documents sampled, the open questions, the responsible party, and the condition required before release. A vague judgment that a site “looked professional” cannot support a sourcing decision. A concise finding such as “final inspection records are retained by lot, but returned material is not linked to its original production record” can be evaluated, corrected, and revisited.
Local supplier audits pay for themselves when they resolve a decision-changing uncertainty before a purchase order turns it into an operational problem. Where the item is easy to replace, technically simple, and supported by proven performance, desk research and normal qualification may be sufficient. Where quality, capacity, outsourced processes, traceability, or recovery time remain uncertain, seeing the operation directly is a rational cost-control measure.
Deep Dive
Related Intelligence
 Cyber SecurityDo High-Net-Worth Buyers Prioritize Cyber Security Certifications When Sourcing Smart HVAC Controllers?Analyst:IT & Security Director
 Cyber SecurityWhat cybersecurity risks arise when integrating POS systems with building management platforms?Analyst:IT & Security Director
 Cyber SecurityHow do cyber security frameworks like NIST CSF apply to smart HVAC control networks in high-rise buildings?Analyst:IT & Security Director