Are Emerging-Market Biodegradable Polymer Suppliers Reliable for Volume Orders?
Key Takeaways
- When does modular construction reduce a project's total cost?Chief Civil Engineer
- What cloud infrastructure analysis reveals about Singapore latency risksIT & Security Director
- How to verify recycled green building materials meet project standardsChief Civil Engineer
- What to evaluate when comparing cybersecurity analysis providersIT & Security Director
- When does agricultural automation equipment pay off for mid-size farms?Agri-Tech Strategist
- How Tank Design Helps Reduce Oxidation Risks in Edible Oil StorageAgri-Tech Strategist
- How to match heavy duty earthmoving equipment to site conditionsChief Civil Engineer
- When chemical supply solutions reduce the risk of production downtimeLead Materials Scientist
Industry Overview
We do not just publish news; we construct a high-fidelity digital footprint for our partners. By aligning with TNE, enterprises build the essential algorithmic "Trust Signals" required by modern search engines, ensuring they stand out to high-net-worth buyers in an increasingly crowded global digital landscape.
Are biodegradable polymer suppliers in emerging markets dependable for volume orders? They can be, but dependability is not a country label or a low-price promise. It is a supplier-specific result of proven operating capacity, secure raw materials, repeatable quality controls, workable logistics, and a contract that makes failure visible and manageable before a large shipment is at risk.
Many buyers make the same early mistake: they compare quoted resin prices and annual nameplate capacity, then assume the supplier with the better number is ready for a multi-container program. Biodegradable polymers are less forgiving than many conventional commodity resins. A small shift in molecular weight, moisture content, additive package, pellet geometry, or drying discipline can change how the material runs on an extrusion, injection molding, thermoforming, or film line.
The practical question is not whether a supplier is located in an emerging market. The real question is whether that specific producer can make your required grade, at your required specification, on a repeatable schedule, with evidence that holds up after the first commercial order.
Are Biodegradable Polymer Suppliers in Emerging Markets Dependable for Volume Orders?
Yes, some are fully dependable for volume orders. Others are suitable only for trials, regional supply, or small recurring purchases. The difference is usually easier to identify than buyers expect, provided they investigate the production system rather than relying on a polished company profile.
A supplier may have modern equipment and technically capable staff yet still be a poor fit for a high-volume export program. Its bottleneck may be imported catalysts, inconsistent agricultural feedstock, limited reactor uptime, restricted working capital, or a logistics route that cannot absorb port disruption. None of those issues means the supplier lacks potential. They do mean that a buyer should not treat a successful sample shipment as proof of scalable supply.
For volume orders, reliability has three parts: the supplier must be able to make the material, release it consistently, and deliver it when the buyer needs it. Missing any one of those creates a procurement problem.
Start With the Grade, Not the Supplier’s Sustainability Story
“Biodegradable polymer” is a broad commercial label, not a single material category. Polylactic acid (PLA), polybutylene adipate terephthalate (PBAT), polyhydroxyalkanoates (PHA), starch blends, cellulose-based compounds, and other formulations behave differently in production and disposal conditions. A supplier can be credible in one chemistry and unreliable in another.
Before assessing a factory, define the material requirement in operational terms. That means identifying the processing method, target melt flow or rheology range where relevant, mechanical properties, heat resistance, color, permitted additives, intended end use, packaging requirements, and acceptable batch-to-batch variation. If the product will contact food, enter a regulated market, or carry a compostability claim, the applicable compliance documents need to be identified at the start.
A broad request such as “we need compostable pellets for packaging” encourages vague quotations. A useful request is closer to: a specified grade for blown film, target thickness range, defined seal performance, agreed moisture limit on delivery, and certificates required for the destination market. The more precise the request, the easier it is to distinguish a true manufacturer from a trader relaying generic specifications.
Do not assume that a certificate held by the supplier automatically covers the exact grade, formulation, product application, or market you plan to serve. Ask for the certificate scope, validity, issuing body, and the specific material identity. Claims about biodegradation are particularly vulnerable to overgeneralization. Industrial compostability, home compostability, soil degradation, and marine degradation are not interchangeable claims.
Capacity Is More Than a Number on a Datasheet
Annual capacity is useful context, but it is not the capacity available to you. A producer may operate several lines, allocate output to existing customers, run campaigns for different grades, or reserve material for its domestic market. The relevant figure is sustainable spare capacity for your grade after normal maintenance, quality holds, and current customer commitments.
Ask direct questions:
- What was the average monthly output for this exact grade during the past six to twelve months?
- How much of that output was exported, and to which types of destinations?
- What is the normal production lead time after a purchase order?
- Can the grade be produced continuously, or only during scheduled campaigns?
- What happens if a batch fails internal release testing?
- Which input materials are imported, and what alternative sources are qualified?
A dependable supplier can answer these questions with operating information, even if some customer names must remain confidential. A weak response often sounds impressive but stays abstract: “large capacity,” “stable production,” or “many overseas clients.” Those statements do not establish whether the manufacturer can reserve two or four monthly shipments for your program.
There is also a difference between nameplate capacity and proven throughput. Nameplate capacity describes what a line may produce under stated conditions. Proven throughput reflects actual output after maintenance, conversion losses, grade changes, quality rejects, and utility constraints. For a volume commitment, proven throughput is the number that matters.
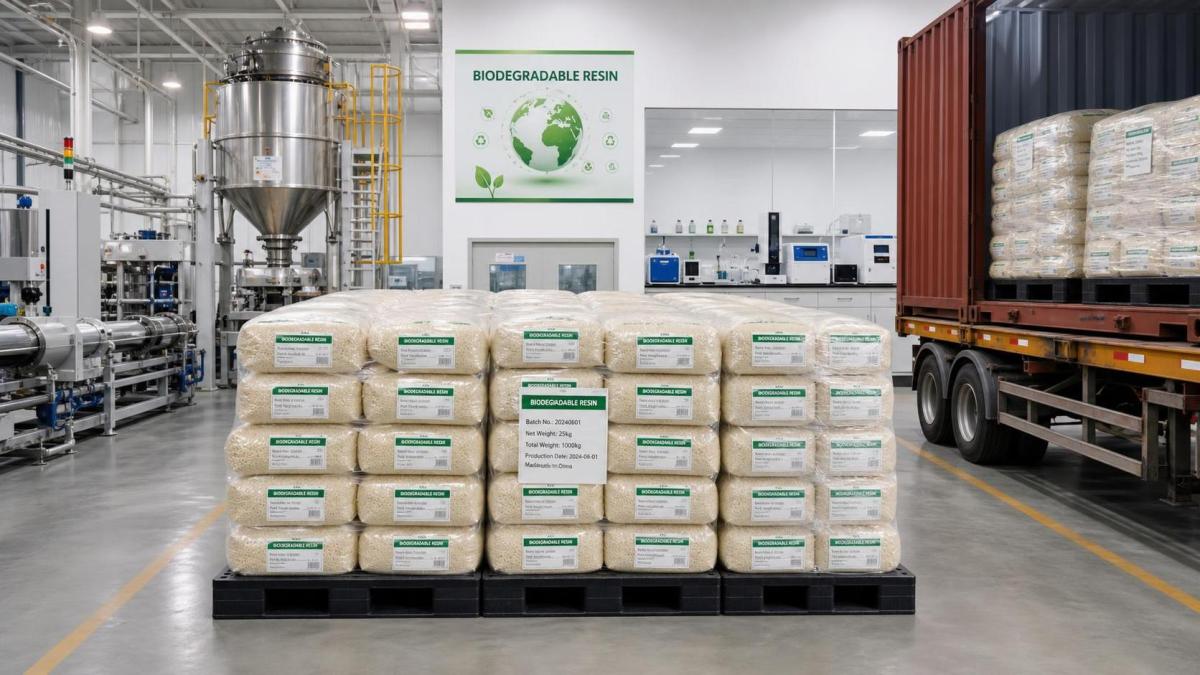
The Best Early Test Is Consistency Across Batches
Buyers often invest heavily in evaluating the first sample. That sample matters, but it is commonly prepared from a favorable batch and may not represent normal production variation. A more useful qualification process compares multiple batches produced at different times.
Request certificates of analysis for recent lots, not just a template. Compare the reported values against the agreed specification and look for drift. Then run conversion trials with material from more than one lot if the application is sensitive. Film processors, for example, should watch for changes in bubble stability, gauge control, haze, odor, blocking, seal behavior, and scrap rate. Molded products may reveal variation through cycle time, warpage, brittleness, surface finish, or dimensional stability.
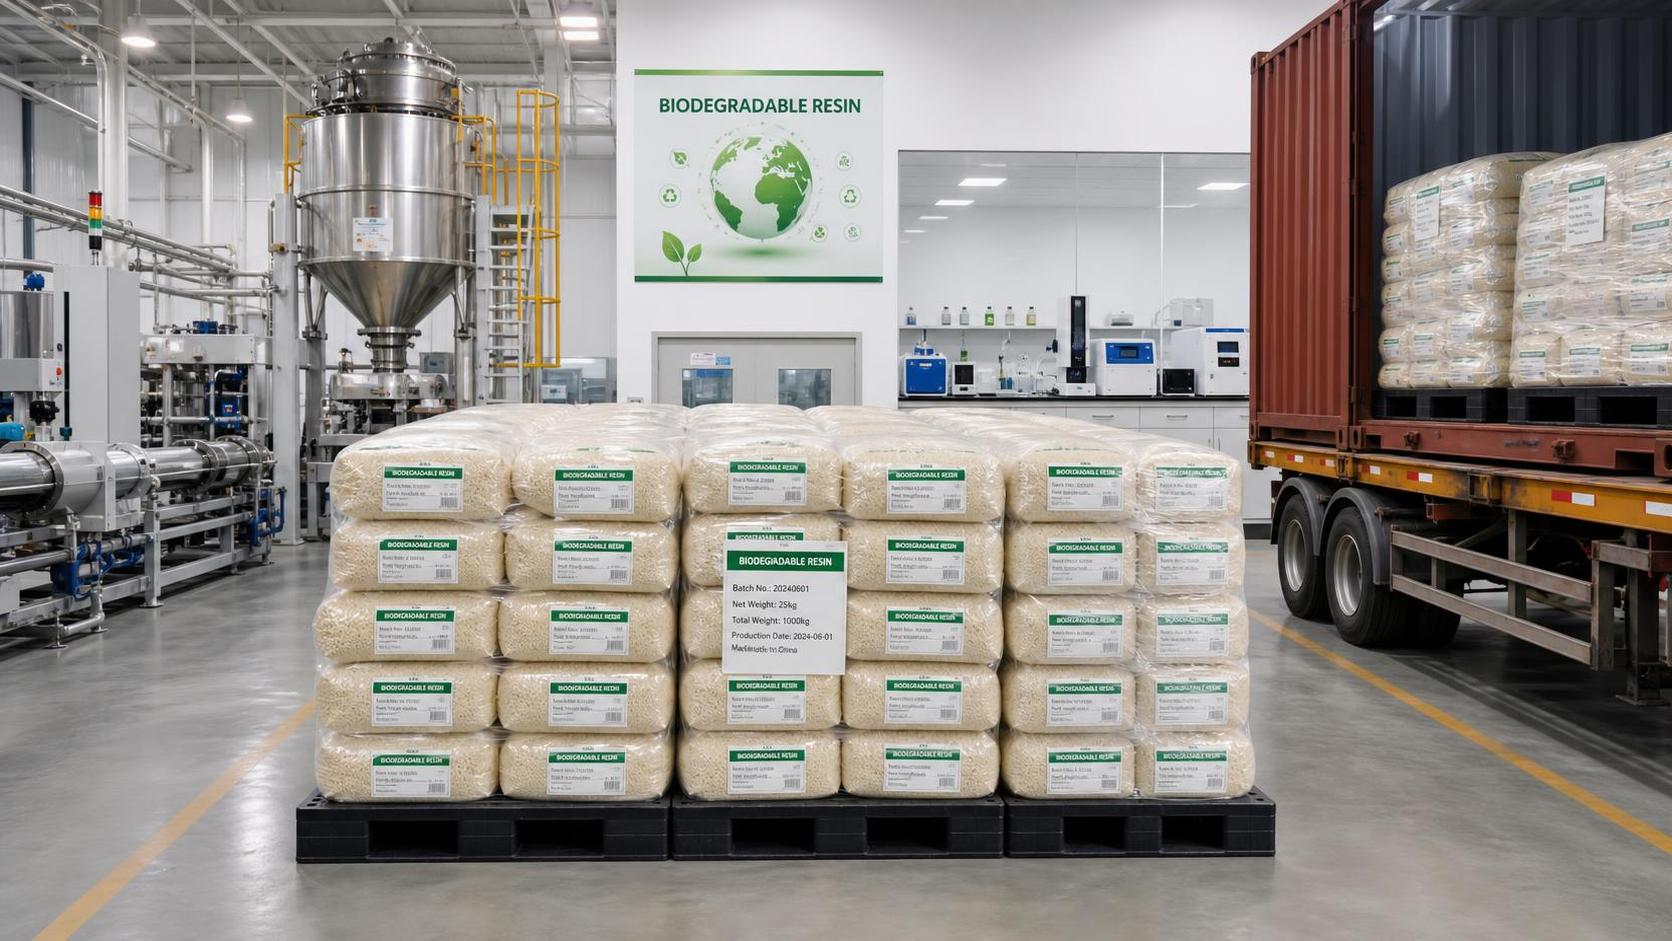
Quality consistency also depends on what happens after the pellets leave the reactor or compounding line. Hygroscopic materials can lose processing stability if drying, storage, bagging, or container loading is poorly controlled. Ask about moisture testing, bag barriers, pallet protection, warehouse conditions, lot traceability, and the procedure for managing nonconforming material.
A supplier that welcomes a documented incoming-quality agreement is usually easier to work with than one that insists its standard specification should settle every issue. The agreement should define the test method, sampling approach, acceptance range, retain-sample period, reporting format, and the process for investigating a disputed lot. “Within spec” is not enough if the supplier and buyer use different test methods or interpret limits differently.
Feedstock Security Can Be the Hidden Risk
Emerging-market producers may have a strong advantage when they are close to local agricultural inputs, fermentation feedstocks, or regional conversion demand. That advantage can reduce transport exposure and support competitive economics. It can also create concentration risk if the producer depends on one crop, one processor, one imported monomer, or one government-controlled utility.
Feedstock risk is not a reason to dismiss the supplier. It is a reason to ask how disruption is handled. Can the factory qualify alternatives without changing the performance of the grade? Does it hold safety stock? Does it have approved second sources? Are key inputs bought on spot markets or under longer-term supply arrangements? The supplier does not need to disclose every commercial term, but it should be able to explain its continuity plan clearly.
This is where buyers should avoid a common misconception: local raw materials do not automatically mean secure raw materials. Availability can vary by season, weather, export rules, competing demand, and transport infrastructure. The same caution applies to suppliers whose production relies on imported intermediates. A low resin price can become expensive when a supply interruption forces urgent substitution, line requalification, or missed delivery dates.
Verify the Factory, the Documents, and the Export Routine
A remote audit is better than no audit, but it should be structured. Request a live walkthrough that shows raw-material receipt, production equipment, laboratory testing, finished-goods storage, batch labeling, and loading procedures. Ask the team to show the date and lot numbers in real time. Pre-recorded videos are useful supporting material, not sufficient verification on their own.
For a larger commitment, an independent third-party audit can be sensible. The scope should match the risk: manufacturing capability, quality management, environmental and safety controls, traceability, labor practices where relevant, and export readiness. It is also sensible to check corporate registration, authorized signatories, bank details, export history where accessible, and whether the entity receiving payment is the entity operating the plant.
Documents require the same discipline. Review the technical data sheet, safety documentation, certificates of analysis, compliance declarations, and any compostability or food-contact documents against the destination market and intended application. Do not accept a logo, a marketing statement, or an expired certificate as equivalent to valid coverage. Regulatory conclusions should be confirmed with qualified local compliance advisers when the application is regulated.
TradeNexus Edge can be useful at this stage as a research starting point for procurement teams comparing materials-market intelligence, supply-chain context, and technical developments. It should support due diligence, not replace factory verification, laboratory testing, or legal and regulatory review.
Logistics Reliability Must Be Designed Into the Order
A capable manufacturer can still fail a volume program through poor export execution. Confirm which port is used, how material moves from the plant to port, typical transit lanes, container availability, pallet configuration, moisture protection, shipping documents, and responsibility under the agreed Incoterms. For moisture-sensitive resin, ask whether desiccants, liners, or other protective measures are appropriate for the route and season.
Build a practical inventory buffer rather than expecting a new supplier to perform like a long-established local distributor on day one. The right buffer depends on consumption, lead time, requalification difficulty, and the cost of a production stoppage. For critical applications, maintaining an approved secondary source is often more valuable than negotiating a marginally lower unit price.
It also helps to separate the commercial order from the supply plan. A twelve-month agreement may set a volume framework, while monthly releases, forecast windows, and firm-order cutoffs determine what the factory must actually produce. This gives both sides a way to manage demand changes without turning every forecast revision into a dispute.
Use a Qualification Ladder Before Committing Full Volume
The safest route is rarely “sample, then annual contract.” A staged approach gives the buyer evidence while giving the supplier a fair opportunity to demonstrate performance.
- Review technical fit and documentation for the exact intended application.
- Test samples and define measurable acceptance criteria.
- Purchase a pilot lot from normal production, not a laboratory batch.
- Compare at least two production lots and record processing results.
- Place a limited commercial order with clear quality, delivery, and claim terms.
- Increase the allocation only after the supplier has met repeated delivery and quality commitments.
This takes more effort than choosing the lowest quoted offer. It also reduces the risk of discovering an avoidable variation problem after your own customers have received finished goods.
What Contract Terms Actually Protect the Buyer?
Contracts cannot manufacture resin or clear a delayed vessel, but they can make responsibilities clear. State the grade identity, technical specification, agreed test methods, packaging, labeling, documentation, Incoterms, lead time, delivery window, inspection procedure, claims period, replacement or credit process, and rules for material changes. A change-control clause is particularly important. The supplier should not alter a feedstock source, additive package, production site, or meaningful processing parameter without notice and, where needed, requalification.
For early orders, payment terms should reflect the stage of trust and the buyer’s leverage. Avoid treating an attractive discount as compensation for accepting unmanageable prepayment risk. Commercial and legal advisers should review the final arrangement, especially where cross-border enforcement, product claims, or regulated end uses are involved.
FAQ
Is an ISO certificate enough to approve a biodegradable polymer supplier?
No. A management-system certificate may indicate that documented processes exist, but it does not prove that your exact grade performs consistently, that claimed certifications apply to your application, or that the supplier can reserve export capacity.
Should a buyer require an on-site audit before the first order?
For low-risk trials, a live remote audit and document review may be proportionate. For strategic material, high annual spend, regulated use, or a supplier with limited export history, an on-site or independent audit is usually justified.
Can a trading company be a reliable source?
Yes, particularly when it adds local stock, technical support, credit terms, or logistics control. The buyer still needs visibility into the actual producer, manufacturing location, batch traceability, and who accepts responsibility for a quality claim.
What is the clearest warning sign during supplier qualification?
Inconsistent answers about the exact grade, recent production history, feedstock origin, or certificate scope deserve attention. Another warning sign is pressure to move directly from a small sample to a large prepaid order.
A Practical Decision, Not a Geographic Bet
Buyers asking whether biodegradable polymer suppliers in emerging markets are dependable for volume orders should avoid both extremes. It is inaccurate to assume that lower-cost regions cannot meet demanding standards. It is equally risky to assume that a modern website, a favorable quotation, and one successful trial prove long-term reliability.
Approve suppliers on evidence: repeat-batch performance, realistic spare capacity, resilient inputs, verified documentation, export discipline, and a contract built around measurable obligations. When those elements are in place, an emerging-market producer can become a strong long-term supply partner. When they are absent, the lower purchase price is usually a warning that the buyer has not yet priced the real risk.
Deep Dive
Related Intelligence
 Eco-PolymersCan Editorial Framework Standards Improve Traceability for Eco-Polymers in Food Packaging?Analyst:Lead Materials Scientist
 Eco-PolymersCan Graphene Materials Deliver Cost-Effective Conductivity in Large-Scale Flooring Projects?Analyst:Lead Materials Scientist
 Eco-PolymersGraphene Materials Bulk Order Thresholds: When Does Unit Cost Drop Below $180/kg for Structural Reinforcement?Analyst:Lead Materials Scientist