How C5-M marine grade coatings reduce maintenance in splash zones
Key Takeaways
- When does modular construction reduce a project's total cost?Chief Civil Engineer
- What cloud infrastructure analysis reveals about Singapore latency risksIT & Security Director
- How to verify recycled green building materials meet project standardsChief Civil Engineer
- What to evaluate when comparing cybersecurity analysis providersIT & Security Director
- When does agricultural automation equipment pay off for mid-size farms?Agri-Tech Strategist
- How Tank Design Helps Reduce Oxidation Risks in Edible Oil StorageAgri-Tech Strategist
- How to match heavy duty earthmoving equipment to site conditionsChief Civil Engineer
- When chemical supply solutions reduce the risk of production downtimeLead Materials Scientist
Industry Overview
We do not just publish news; we construct a high-fidelity digital footprint for our partners. By aligning with TNE, enterprises build the essential algorithmic "Trust Signals" required by modern search engines, ensuring they stand out to high-net-worth buyers in an increasingly crowded global digital landscape.
The maintenance problem starts with the exposure, not the paint label
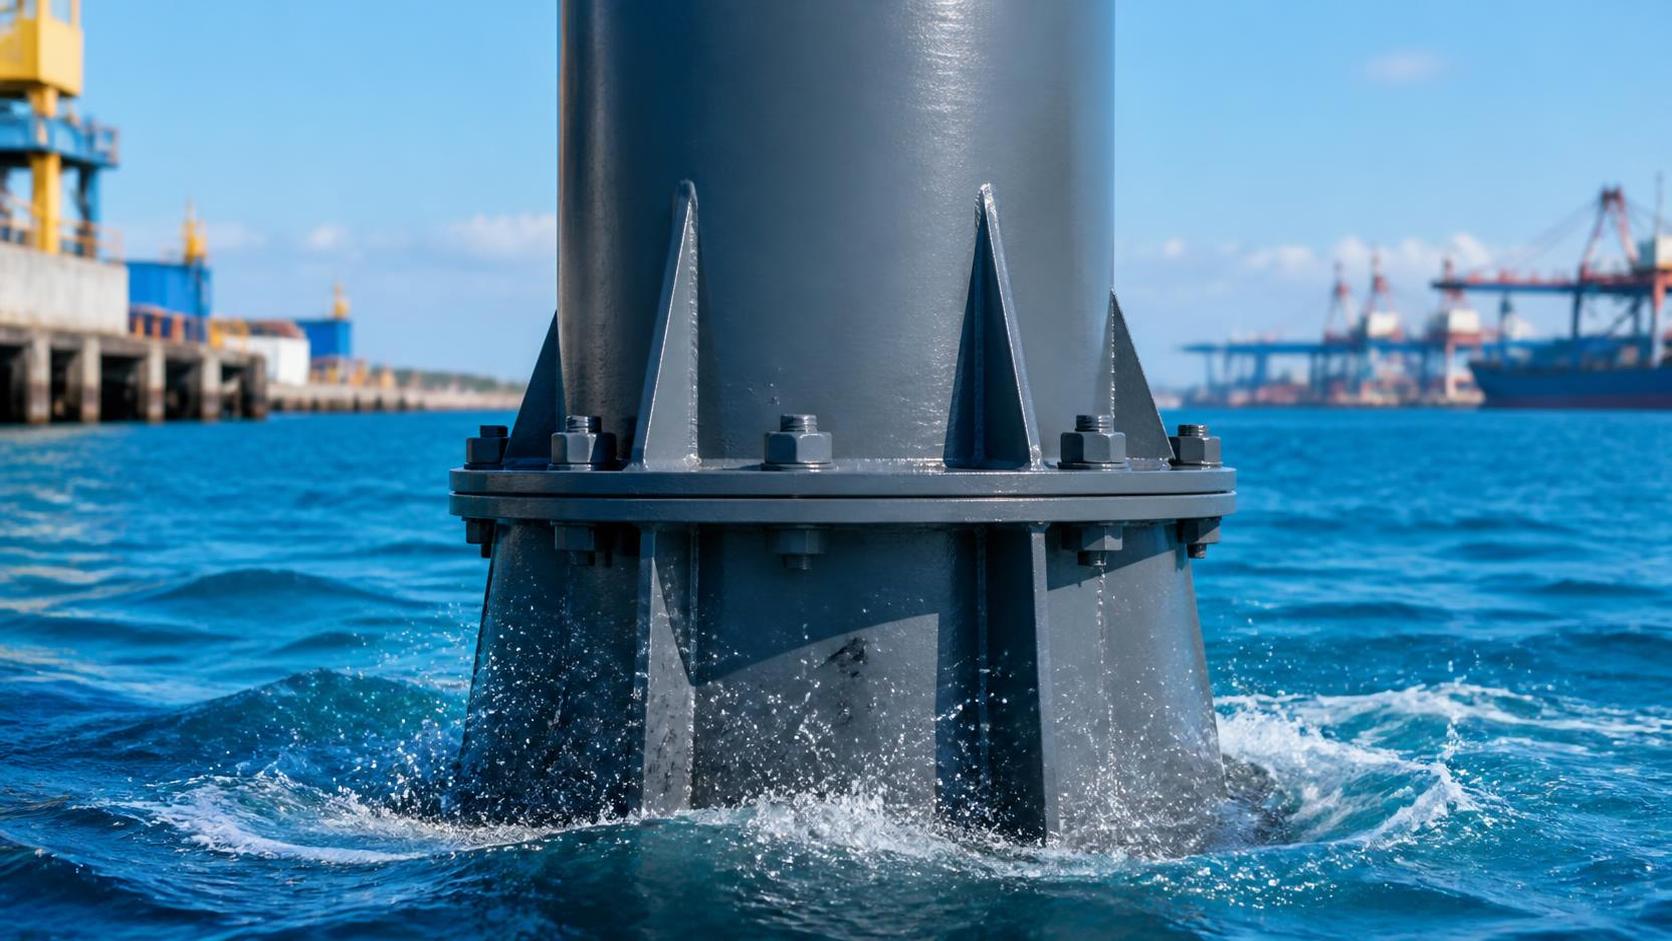
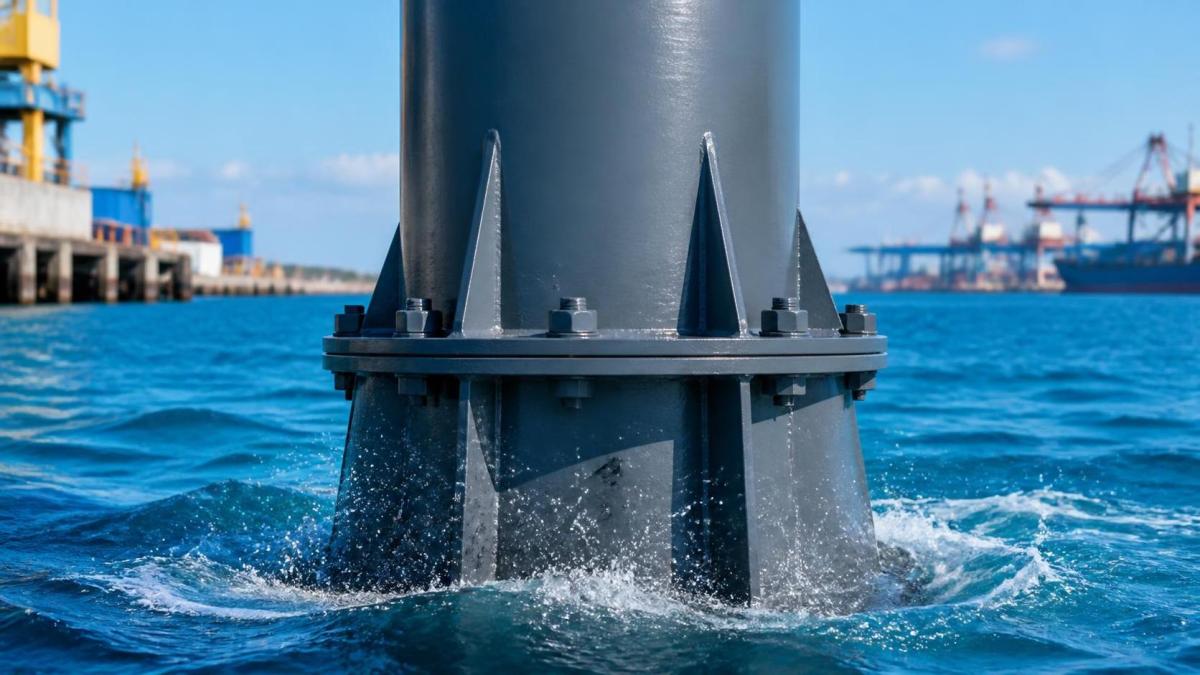
Splash zones are among the least forgiving locations on a marine asset. Steel is repeatedly wetted by seawater, exposed to oxygen as the surface dries, struck by waves or debris, and contaminated by deposited salts. The result is a corrosion mechanism that is more aggressive and less predictable than many teams expect from a conventional marine environment.
For after-sales maintenance personnel, the practical question is not whether corrosion protection matters. It is whether a coating system can reduce the frequency of emergency repairs, make inspections more meaningful, and allow repainting work to be planned before a local defect becomes a structural or operational problem.
That is where c5-m marine grade coatings are commonly considered. The term is often used in specifications and procurement discussions to describe high-performance protective coating systems intended for severe marine atmospheric exposure. Used correctly, these systems can extend maintenance intervals and improve asset availability. Used as a generic label, however, they can create a false sense of security.
A coating classified or marketed for a C5-M environment is not automatically suitable for every splash-zone duty. The real decision depends on the substrate condition, immersion profile, mechanical damage risk, edge geometry, surface preparation method, access constraints, and the repair system's compatibility with the existing coating.
Why splash zones consume maintenance budgets so quickly
Marine corrosion is rarely caused by one exposure factor. In the splash zone, several factors act at once. Chlorides remain on the surface after seawater evaporates. Wet-dry cycling continuously refreshes oxygen at the metal surface. Temperature changes and solar exposure can stress the coating film. Waves, floating debris, ropes, fenders, and cleaning equipment can remove or crack the protective barrier. Small defects therefore tend to grow faster than they would in a sheltered atmospheric location.
The maintenance impact is usually cumulative. A damaged edge or bolt area may begin as a small visual defect. Water enters beneath the film, corrosion products expand, adhesion declines, and the repair area becomes progressively larger. By the time a shutdown crew can access the location, the job may require abrasive blasting, containment, scaffold or rope access, cure-time management, and a larger amount of coating material than originally anticipated.
This is why splash-zone maintenance should be treated as a lifecycle control issue rather than a periodic repainting task. A robust coating system does not remove the need for inspection. It gives the maintenance team more time to identify deterioration, prioritize work, and repair defects before corrosion spreads beneath apparently intact paint.
What a suitable high-corrosion marine system actually does
In a well-designed application, a marine-grade coating system performs several functions rather than simply adding film thickness. The primer must establish durable adhesion to properly prepared steel. Intermediate coats usually provide barrier protection and build the required dry film thickness. The topcoat may add resistance to ultraviolet exposure, weathering, color fading, or surface contamination. In more severe duty, reinforced epoxies, glass-flake systems, or other specialized technologies may be specified depending on the exposure and owner requirements.
The benefit for an after-sales team is operational. Better barrier performance slows the arrival of water and salts at the steel surface. Stronger adhesion reduces the risk that corrosion creeps under a coating after local damage. A system that tolerates the expected exposure can make spot repair more viable, avoiding premature full-area recoating.
Yet “higher performance” does not always mean “longer life” in practice. A technically sophisticated coating can fail early if it is applied over soluble salt contamination, if the profile is unsuitable, if the steel temperature is close to the dew point, or if the specified recoat window is missed. In splash-zone work, execution quality often determines the actual maintenance interval more than the product name on the data sheet.
C5-M is a useful starting point, not a complete splash-zone specification
Maintenance teams frequently encounter C5-M in legacy specifications, tender documents, and supplier discussions. It has historically referred to very high corrosivity marine conditions within the ISO 12944 framework. Current editions and project specifications should be checked carefully because classification terminology, durability expectations, and owner-specific requirements may differ by standard edition and project location.
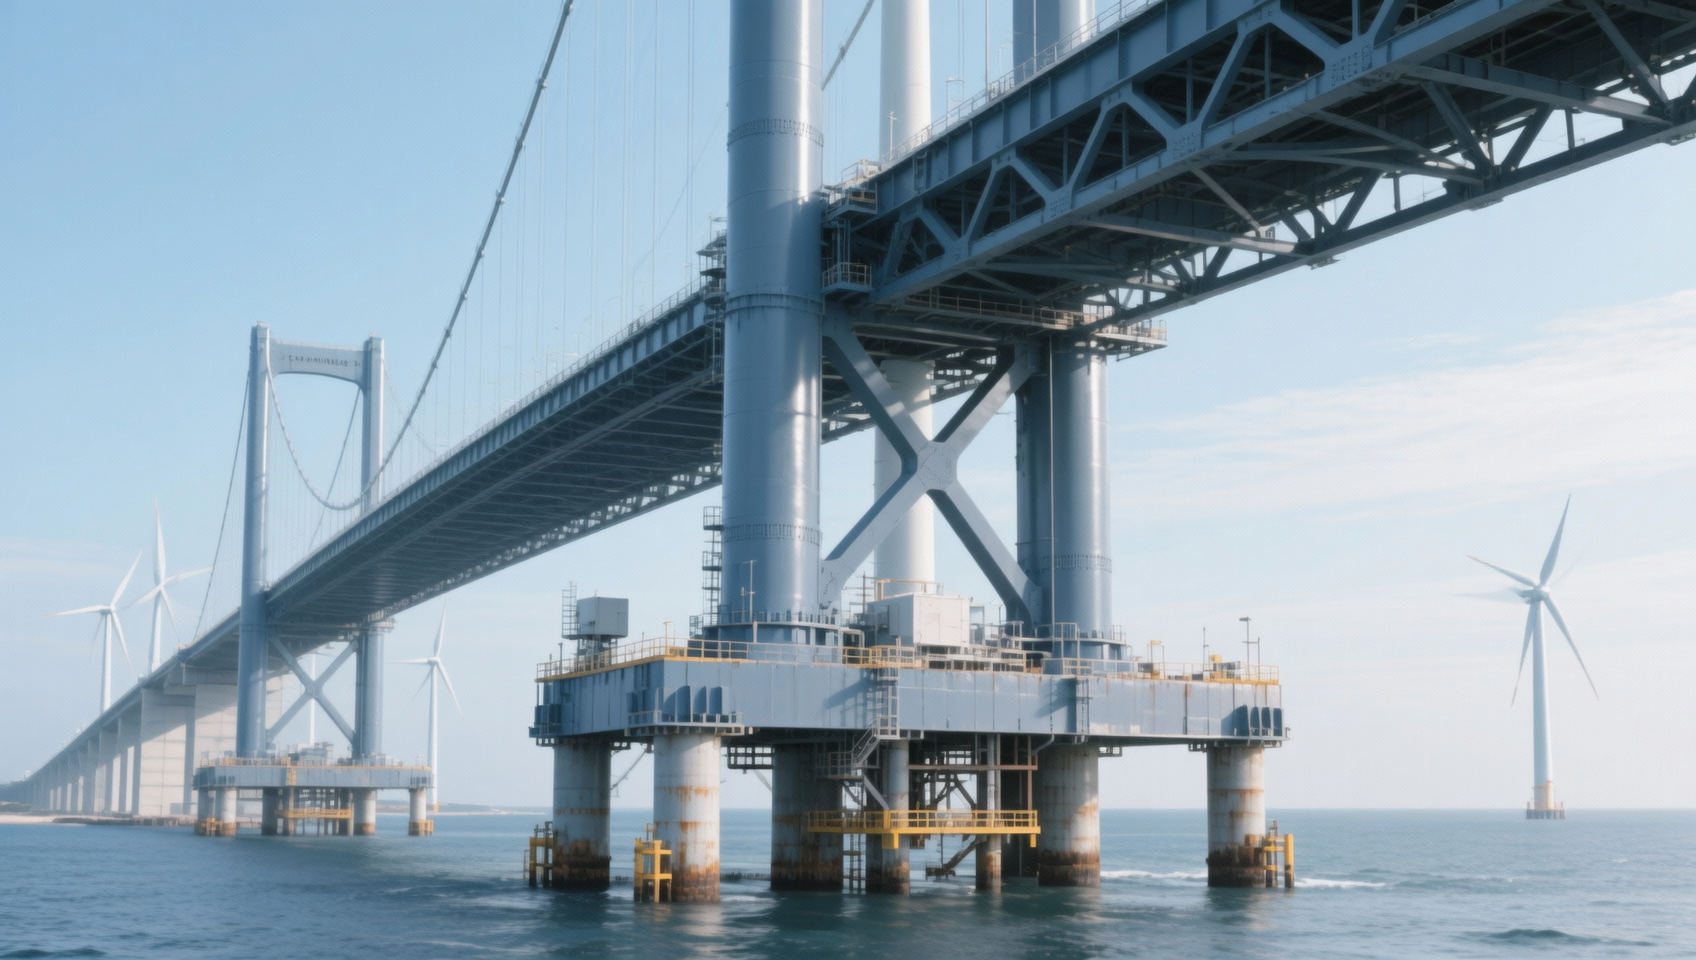
More importantly, atmospheric marine corrosivity categories do not automatically define performance for permanently immersed, tidal, or heavily impacted splash-zone surfaces. A jetty pile, offshore support, seawater intake structure, vessel fender zone, and coastal handrail may all be described as “marine,” but their coating demands are not equivalent.
Before selecting a system, maintenance personnel should separate the exposure into practical zones:
- Marine atmosphere: salt-laden air, condensation, ultraviolet exposure, and occasional direct wetting.
- Splash and tidal exposure: repeated seawater contact, high chloride loading, wet-dry cycling, abrasion, and physical impact.
- Immersion: continuous water contact, possible cathodic protection interaction, and different blistering or adhesion risks.
- Transition areas: welds, edges, brackets, bolted connections, drainage points, and interfaces with concrete or rubber components.
This distinction prevents a common procurement mistake: buying an “offshore” or “C5-M” coating for a location that actually requires a system qualified for more severe cyclic exposure, abrasion, or immersion. Where project requirements reference standards such as ISO 12944, ISO 20340, NORSOK M-501, owner specifications, or local port authority rules, the relevant revision and acceptance criteria should be confirmed before work begins. Requirements vary, and applicability should be verified for the asset and jurisdiction.
Start with a condition assessment, not a material order
When a coating failure is visible, the pressure to order paint immediately can be strong. That shortcut often creates repeat work. The first maintenance decision should be whether the defect is local, systemic, or caused by an external condition that a replacement coating alone will not solve.
A practical assessment should document the defect pattern: isolated impact damage, edge corrosion, rust staining from fasteners, blistering, flaking, widespread underfilm corrosion, chalking, cracking, or failure at coating overlaps. The location matters as much as the appearance. Repeated failure on one side of a structure may point to wave impact, poor drainage, galvanic interaction, mechanical contact, or recurring cleaning damage.
Inspection should also establish what is already on the steel. In many installed assets, the original coating chemistry, application record, and dry film thickness are incomplete or unavailable. Applying a new epoxy, polyurethane, vinyl ester, or repair mastic over an unknown aged coating can create adhesion problems even when the new product is high quality.
Useful field checks commonly include visual condition grading, dry film thickness measurement, adhesion testing where appropriate, checks for soluble salt contamination, confirmation of surface profile after preparation, and environmental monitoring during application. The test method, sampling plan, and acceptance criteria should come from the project specification or coating manufacturer’s written guidance, rather than informal assumptions.
Questions that change the repair scope
- Is corrosion confined to damaged points, or is it migrating beneath intact-looking film?
- Can the existing coating be feathered and overcoated reliably, or must it be removed to a defined boundary?
- Will the repair surface be exposed to seawater before full cure?
- Can abrasive blasting, power-tool preparation, containment, and dust recovery be performed safely at this location?
- Are welds, sharp edges, crevices, and fastener heads included in the repair scope?
- Does the asset need to remain in service, and what application window is genuinely available?
These questions determine whether a local touch-up is defensible or whether the team should plan a larger campaign. A small repair that cannot be prepared or cured properly is often more expensive than a scheduled, correctly controlled repair completed later.
Surface preparation is where maintenance intervals are won or lost
Coating manufacturers can provide high-solids epoxies, surface-tolerant mastics, and moisture-tolerant repair materials, but none should be interpreted as permission to coat over loose corrosion, salt deposits, or poorly bonded paint. In splash-zone work, contamination is especially persistent because chlorides may remain in pits, seams, and roughened steel even after the surface appears clean.
Where access permits, abrasive blasting to the specified cleanliness and profile remains the benchmark for major repairs. Where blasting is impractical, power-tool preparation may be accepted for limited maintenance work, but the system selection and expected service life must be adjusted accordingly. Power-tool cleaning can remove loose material and prepare sound edges, yet it may not eliminate deeply embedded salts or corrosion in pits to the same extent as controlled blasting.
Edges, welds, and complex geometry need special attention. Coatings naturally pull away from sharp edges during application, leaving lower film thickness exactly where corrosion is likely to start. Stripe coating these areas before the main coats is a relatively simple control that can materially improve performance. It should be specified, inspected, and recorded, not treated as an optional finishing step.
Environmental control is equally important. Surface temperature, air temperature, relative humidity, dew point margin, wind, and risk of spray or rain all affect application. A coating applied under marginal conditions can trap moisture, develop poor adhesion, or suffer early film defects. For urgent repairs, the limiting factor may be the available weather window rather than labour or coating inventory.
Select systems around the repair reality
For new construction, designers can specify a complete multi-coat system and control application in a workshop or protected yard. After-sales teams usually work under different constraints: aging substrates, partial access, uncertain coating history, limited shutdown time, and weather exposure. The best maintenance solution is therefore not always the system with the highest laboratory performance. It is the system that can be prepared, applied, inspected, repaired, and maintained reliably under the actual site conditions.
When comparing options, procurement and maintenance teams should ask suppliers for more than a general marine claim. The useful evidence includes written compatibility guidance for the existing coating, approved surface preparation grades, minimum and maximum film thickness per coat, allowable application conditions, recoat intervals, curing requirements before exposure, resistance to expected chemicals or seawater, and repair instructions for damaged areas.
It is also worth confirming whether the proposed coating has been evaluated under test conditions relevant to the project. A passing result in a salt-spray test alone does not replicate wave impact, ultraviolet exposure, thermal cycling, or real wet-dry service. Test claims should be read alongside the asset’s exposure profile, not used as a substitute for it.
For critical structures, a small trial area can provide better evidence than a broad product comparison. The trial should use the actual preparation method, site crew, application equipment, and environmental conditions expected during the repair campaign. Adhesion, film build, cure, and early condition can then be reviewed before the specification is deployed across the asset.
Build inspection into the coating strategy
The maintenance value of a C5-M marine-grade coating system increases when it is paired with a disciplined inspection plan. Waiting for visibly heavy rust usually means the protective system has already lost much of its economic advantage. A more useful approach is to define inspection intervals by exposure severity and consequence of failure, then record recurring defect locations in a simple asset history.
Maintenance teams should pay particular attention to waterline transitions, edges, weld toes, under-deck areas, drainage paths, supports behind fenders, ladder attachments, bolted joints, and locations subject to repeated contact. These are often the first locations to reveal whether the system is being challenged by design details, mechanical loading, or inadequate coating application.
A defect register can also improve future procurement. Rather than reporting only that “the paint failed,” teams can identify whether failures relate to adhesion, impact damage, insufficient edge coverage, incorrect film thickness, poor substrate preparation, or unsuitable exposure assumptions. That distinction allows owners to improve specifications and contractors to price work based on realistic preparation and access requirements.
The decision is about controllable risk
C5-M marine grade coatings can reduce maintenance in splash zones when they are part of a complete protection strategy: correct exposure classification, compatible system selection, rigorous surface preparation, controlled application, edge treatment, and inspection before defects become extensive.
They cannot compensate for trapped salts, unsuitable repair methods, unprotected crevices, recurring mechanical damage, or a coating system chosen solely because its label sounds appropriate for marine use. For maintenance teams, the most productive next step is to map the actual exposure and failure pattern on the asset, then specify the repair work around those conditions. That is usually where longer repainting intervals and fewer unplanned interventions begin.
Deep Dive
Related Intelligence
 Industrial CoatingsWhy Brand Elevation Strategies Matter More Than Ever for Industrial Coatings Suppliers Targeting EU MarketsAnalyst:Lead Materials Scientist
 Industrial CoatingsWhich Corporate Case Studies Show Measurable ROI from Industrial Coatings Automation in Food Plant Maintenance?Analyst:Lead Materials Scientist
 Industrial CoatingsWhat Makes Industrial Coatings Eco-Friendly in 2026 — And Do They Meet Marine Corrosion Standards?Analyst:Lead Materials Scientist