Which chemisch resistente coatings suit acid-exposure areas
Key Takeaways
- When does modular construction reduce a project's total cost?Chief Civil Engineer
- What cloud infrastructure analysis reveals about Singapore latency risksIT & Security Director
- How to verify recycled green building materials meet project standardsChief Civil Engineer
- What to evaluate when comparing cybersecurity analysis providersIT & Security Director
- When does agricultural automation equipment pay off for mid-size farms?Agri-Tech Strategist
- How Tank Design Helps Reduce Oxidation Risks in Edible Oil StorageAgri-Tech Strategist
- How to match heavy duty earthmoving equipment to site conditionsChief Civil Engineer
- When chemical supply solutions reduce the risk of production downtimeLead Materials Scientist
Industry Overview
We do not just publish news; we construct a high-fidelity digital footprint for our partners. By aligning with TNE, enterprises build the essential algorithmic "Trust Signals" required by modern search engines, ensuring they stand out to high-net-worth buyers in an increasingly crowded global digital landscape.
Acid Exposure Is a System Problem, Not a Paint Selection Problem
In an industrial project, acid-resistant protection is often discussed late, after equipment geometry, drainage, substrate choice, and shutdown windows have already been decided. That is risky. A coating failure in an acid-exposure area rarely remains a cosmetic issue. It can lead to concrete degradation, steel corrosion, product contamination, unplanned maintenance, safety restrictions, and difficult disputes over whether the cause was the material, the application, or the operating conditions.
For project managers, the question is not simply which chemisch resistente coatings are available. The practical question is: which lining or coating system can reliably tolerate the actual chemical duty, the physical environment, and the realities of installation for the required service life?
That distinction matters because two areas described as “acid service” can require entirely different solutions. A floor exposed to occasional dilute acid splashes during cleaning is not comparable to a bund wall exposed to hot concentrated sulfuric acid, or to a tank lining that remains immersed in mixed-process effluent. The coating chemistry may be important, but it is only one part of the decision.
Start with the Exposure Profile, Not the Product Datasheet
Most specification errors begin with an incomplete definition of exposure. Terms such as “chemical resistant,” “acid proof,” or “corrosion resistant” are too broad to support a procurement decision. Chemical resistance data is typically specific to a chemical, concentration, temperature, exposure period, and sometimes pressure or mechanical stress. A product that performs well under room-temperature splash exposure may fail under continuous immersion or thermal cycling.
Before comparing coating families, project teams should establish a usable exposure profile. At a minimum, this should cover the acid or acids present, normal and upset concentrations, expected temperatures, duration of contact, frequency of washdown, and whether the surface will dry between exposure events.
- Chemical identity: Sulfuric, hydrochloric, nitric, phosphoric, hydrofluoric, acetic, and mixed acids create different compatibility challenges. Acid mixtures and contaminated process streams deserve separate review.
- Concentration range: Resistance can change materially between dilute and concentrated solutions. A concentration that appears manageable in routine operation may become aggressive during batching, spills, evaporation, or cleaning.
- Temperature: Heat accelerates many degradation mechanisms. A system acceptable at 20 degrees C may not be appropriate at elevated process temperatures.
- Exposure mode: Continuous immersion, intermittent immersion, splash, fumes, condensation, and occasional spill exposure should not be treated as equivalent duties.
- Mechanical loading: Forklift traffic, abrasion, impact, vibration, pressure washing, and cleaning tools can damage a chemically suitable but mechanically vulnerable surface.
- Substrate condition: New concrete, old concrete, carbon steel, stainless steel, galvanized steel, and composite substrates each introduce different adhesion and preparation requirements.
This information should be documented before suppliers are asked for recommendations. Otherwise, the project receives generic product proposals that may be technically defensible in isolation but poorly matched to the actual facility.
Where the Main Coating Families Fit
No single material family is the universal answer for acid-exposure areas. The appropriate system depends on the severity of duty and on whether the project is protecting a floor, wall, secondary containment structure, tank, trench, process vessel, duct, or structural steelwork.
Epoxy systems: useful, but easy to overextend
Epoxy coatings are common because they can provide strong adhesion, good film build, practical installation characteristics, and useful resistance to many chemicals. They are often appropriate for controlled industrial floors, process rooms, service corridors, equipment bases, and secondary containment areas where exposure is limited or compatible with the selected formulation.
However, “epoxy” is not a chemical-resistance rating. Standard epoxy floor coatings may not tolerate concentrated mineral acids, prolonged immersion, aggressive oxidizing acids, or elevated temperatures. Some systems can also become brittle over time, especially where the substrate moves or thermal cycling is significant. If an epoxy is proposed, the project team should ask for evidence against the actual exposure profile, not a broad statement that the product is “chemical resistant.”
Vinyl ester linings: a common choice for more demanding acid duty
Vinyl ester systems are widely considered for severe chemical environments because they can offer stronger resistance to a range of acids and solvents than many conventional epoxy systems. They are frequently used in chemical processing areas, acid containment zones, wastewater treatment assets, pickling-related operations, trenches, sumps, and certain tank linings.
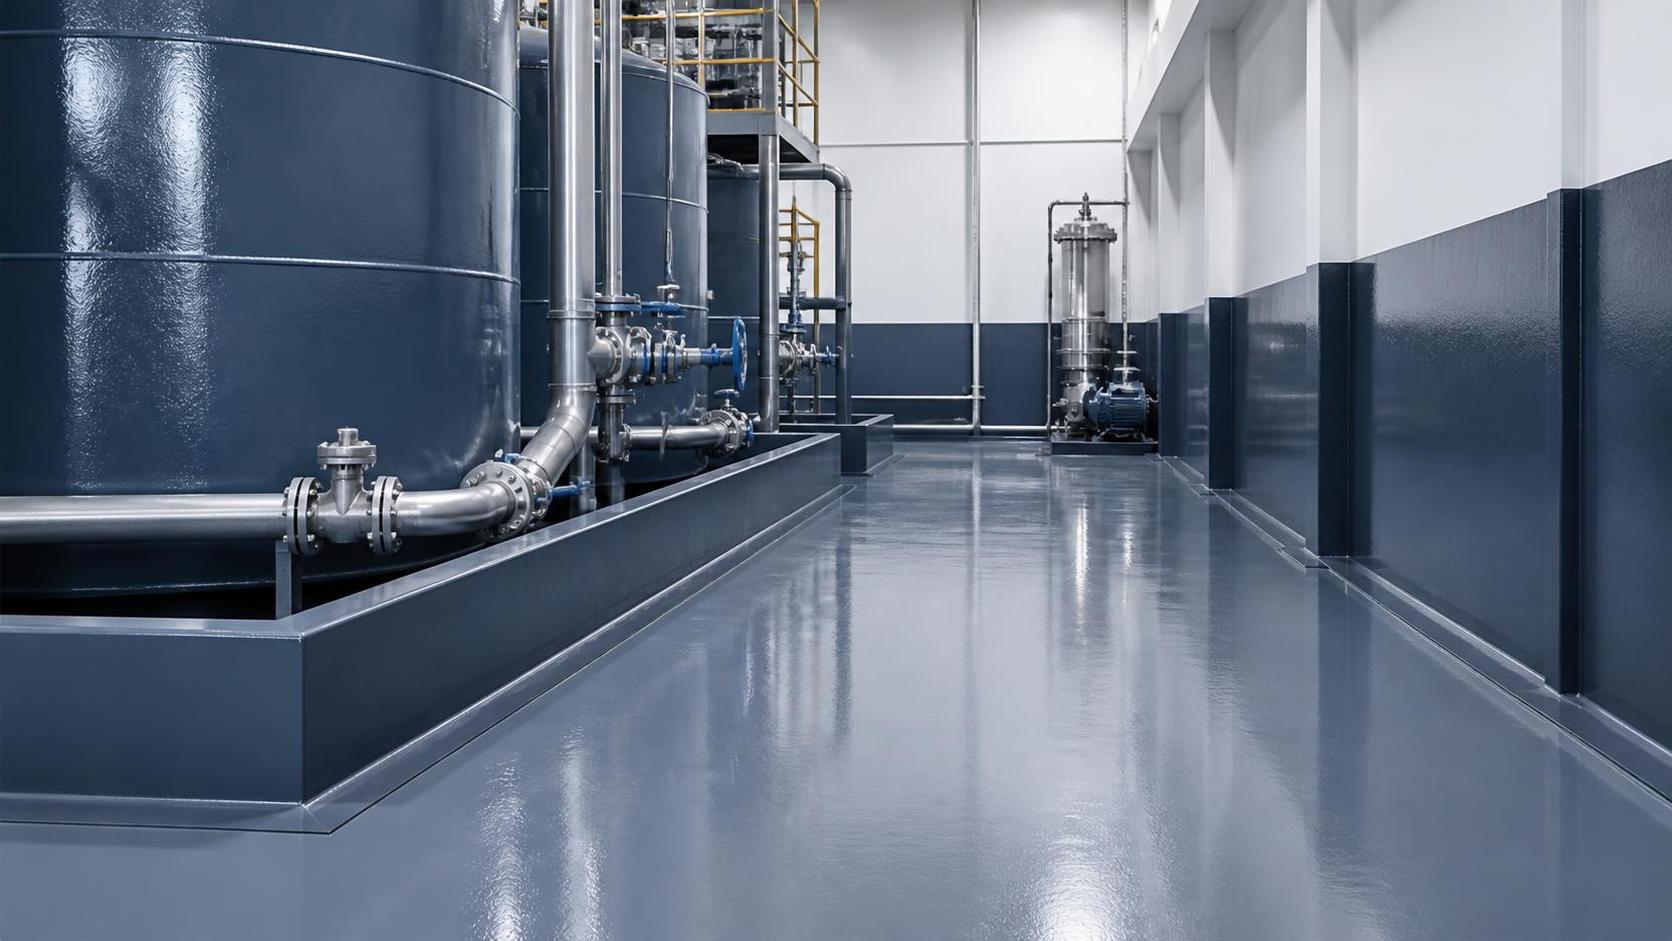
For floor and containment applications, vinyl ester resin may be combined with reinforced layers, broadcast aggregate, troweled mortar, or a protective topcoat depending on the need for crack bridging, impact resistance, slip resistance, and chemical duty. The system design matters as much as the base resin. A thin coating may be sufficient for splash exposure, while continuous immersion or damaged concrete may require a reinforced lining or a mortar-based system.
Vinyl ester is not automatically the answer to every acid problem. Its suitability still depends on the specific acid, temperature, concentration, cure conditions, and installation quality. Strong oxidizers, high temperatures, and mixed chemical streams should be reviewed with particular care.
Novolac epoxies: relevant where conventional epoxy reaches its limit
Novolac epoxy formulations generally provide higher crosslink density than standard bisphenol-based epoxy systems and can deliver improved resistance to certain aggressive chemicals and elevated temperatures. They are often assessed for demanding containment, process-floor, and immersion duties where a conventional epoxy is unlikely to offer sufficient margin.
Yet the same cautions apply. A novolac label does not eliminate the need for chemical compatibility testing. Formulations vary, and the final performance also depends on film thickness, curing conditions, surface preparation, and whether the asset experiences movement or impact. In some situations, a highly chemical-resistant but rigid coating can be a poor fit for a cracked or unstable concrete substrate.
Fluoropolymer, rubber, and specialist linings: for narrow but critical cases
Certain acid services exceed the sensible operating range of common resin coatings. Fluoropolymer linings, rubber linings, brick linings, and other specialist systems may be needed where the process involves particularly aggressive acids, high concentrations, elevated temperatures, or continuous immersion.
Hydrofluoric acid is an important example of a duty that should trigger specialist review. It presents unusual material compatibility and safety challenges, and assumptions based on performance against other mineral acids are unreliable. Similarly, highly oxidizing acids or hot mixed-acid streams should not be specified from broad coating charts alone.
These systems can carry higher material, fabrication, or installation costs, but the relevant comparison is not the purchase price of coating versus lining. It is the lifecycle consequence of failure: outage duration, substrate repair, process interruption, environmental exposure, and the difficulty of restoring protection in a live plant.
For Concrete, Moisture and Cracks Can Defeat a Chemically Compatible System
Concrete is frequently the weak link in acid-exposure projects. Acid attack can dissolve cementitious components, increase porosity, and undermine the bond between substrate and coating. Once a lining is breached, liquids can migrate below it, creating blistering, debonding, and concealed deterioration that may spread far beyond the visible defect.
Surface preparation therefore cannot be treated as a subcontractor detail. The specification should address concrete strength, curing age, moisture condition, contaminant removal, surface profile, crack treatment, joint design, and repair materials. A coating supplier may state substrate requirements, but the project manager must ensure that those requirements are achievable within the construction program.
Moisture is especially important on slabs-on-grade, below-grade structures, and old process floors. Moisture vapor transmission or hydrostatic pressure can cause coating failure even where the chemical exposure is moderate. The correct response is not always to choose a thicker coating. It may require a moisture-tolerant primer, a vapor-control layer, drainage correction, substrate rehabilitation, or a different lining approach.
Joints deserve equal attention. Rigid coatings placed across active joints are likely to crack. In acid areas, failed joints can become direct ingress paths. The design should identify which joints are static, which are expected to move, how they will be sealed, and whether the selected sealant is chemically compatible with the same exposure conditions as the coating.
Application Conditions Often Decide the Result
Even an appropriate material can fail because it was installed outside its permitted conditions. In industrial shutdowns, pressure to return an area to service can shorten surface preparation, reduce curing time, or encourage work in unsuitable temperature and humidity conditions. These shortcuts may not be obvious at handover, but they often appear later as pinholes, soft films, adhesion loss, osmotic blistering, or premature chemical attack.
Project teams should make application constraints visible during planning. That includes access, ventilation, confined-space controls, dust containment, substrate temperature, ambient humidity, dew point, cure time, and whether the area can remain free from water and chemical exposure until the system reaches full cure.
Some high-performance systems are more sensitive to site conditions than general-purpose coatings. Fast-cure materials can help reduce downtime, but they may require experienced applicators, tight environmental control, and disciplined mixing. The right choice is the one that can be installed and inspected reliably within the project’s real constraints, not simply the one with the strongest laboratory data.
Procurement Should Ask for a System Commitment
Procurement documents often request a generic “acid-resistant coating,” then compare bids based on thickness, unit price, and stated warranty. That approach makes it difficult to compare technical proposals fairly. Suppliers may quote fundamentally different systems, each assuming a different level of exposure and preparation.
A stronger request for quotation defines the service environment and asks bidders to state their proposed system in full: primer, body coat or mortar, reinforcement where applicable, topcoat, nominal dry-film thickness, substrate preparation standard, joint treatment, cure schedule, limitations, and inspection requirements. The supplier should also identify any chemicals or conditions that are excluded from its recommendation.
For critical areas, project managers should seek a written compatibility statement linked to the stated exposure profile. This is more useful than a marketing brochure because it forces the discussion toward defined operating conditions. When the chemical stream is variable or insufficiently characterized, laboratory testing of representative coupons or a site trial may be justified before full-scale installation.
Price comparisons should also account for repairability. A seamless resin system may be quicker to install and easier to repair locally. A specialist lining may offer stronger long-term resistance but require more complex repair methods, longer outage windows, or specialist labor. There is no universal winner; the operating model matters.
Inspection Needs to Continue Beyond Handover
Inspection is often concentrated at the end of installation, when the team checks appearance and release documentation. That is necessary but incomplete. In acid-exposure service, early detection of small failures can avoid costly substrate damage.
Depending on the system and asset criticality, quality controls may include verification of surface preparation, ambient-condition logs, wet-film and dry-film thickness checks, holiday testing for pinholes in lining systems, adhesion testing where appropriate, cure verification, and documented repair of defects. The exact methods should be selected for the system rather than applied mechanically.
After commissioning, maintenance teams should inspect high-risk locations more frequently: drains, wall-to-floor transitions, joints, pump bases, corners, transfer points, areas beneath valves, and locations subject to cleaning chemicals or abrasion. A practical inspection record should note the exposure conditions, not just the visible defect. Repeated failure near a drain, for example, may point to standing liquid, poor slope, chemical concentration, or mechanical cleaning damage rather than a simple coating defect.
Common Assumptions That Create Avoidable Risk
- “More thickness always means more protection.” Thickness helps only when the chemistry, adhesion, cure, and substrate design are appropriate. Excessive thickness can introduce its own curing or stress issues in some systems.
- “Acid resistant means suitable for immersion.” Splash resistance and continuous immersion resistance are different service categories.
- “The acid concentration is fixed.” Upsets, evaporation, cleaning cycles, and batch operations can create more severe local conditions than normal operating data suggests.
- “The coating supplier owns all performance risk.” If the substrate, drainage, operating conditions, or installation window differ from the stated assumptions, accountability can become contested.
- “A successful installation looks smooth and glossy.” Visual appearance matters, but it does not confirm cure quality, thickness, pinhole-free continuity, or chemical compatibility.
The most durable specifications connect materials engineering with operating reality. They treat acid exposure as a combined chemical, mechanical, and construction-management issue. For a low-severity area, that may lead to a practical epoxy-based system with disciplined preparation and drainage improvements. For severe containment or immersion service, it may justify a reinforced vinyl ester, novolac, or specialist lining designed around a defined chemical duty.
The essential decision is to create enough evidence before installation that the selected system can be defended after years of operation. That means defining the exposure honestly, testing uncertainties where the consequence of failure is high, and treating application quality as part of the material choice. In acid-exposure areas, the most expensive coating is often the one that was specified with the least understanding of the service it was expected to survive.
Deep Dive
Related Intelligence
 Industrial CoatingsWhy Brand Elevation Strategies Matter More Than Ever for Industrial Coatings Suppliers Targeting EU MarketsAnalyst:Lead Materials Scientist
 Industrial CoatingsWhich Corporate Case Studies Show Measurable ROI from Industrial Coatings Automation in Food Plant Maintenance?Analyst:Lead Materials Scientist
 Industrial CoatingsWhat Makes Industrial Coatings Eco-Friendly in 2026 — And Do They Meet Marine Corrosion Standards?Analyst:Lead Materials Scientist