Livestock & Poultry Tech
How Feed Delivery System Specifications Influence Total Equipment Cost for Medium-Scale Poultry Farms
poultry farm equipment price list: Discover how feed delivery system specs—material, control, IP rating & more—directly impact total cost for medium-scale poultry farms.
Analyst :Agri-Tech Strategist
Sep 16, 2026
Key Takeaways
- When does modular construction reduce a project's total cost?Chief Civil Engineer
- What cloud infrastructure analysis reveals about Singapore latency risksIT & Security Director
- How to verify recycled green building materials meet project standardsChief Civil Engineer
- What to evaluate when comparing cybersecurity analysis providersIT & Security Director
- When does agricultural automation equipment pay off for mid-size farms?Agri-Tech Strategist
- How Tank Design Helps Reduce Oxidation Risks in Edible Oil StorageAgri-Tech Strategist
- How to match heavy duty earthmoving equipment to site conditionsChief Civil Engineer
- When chemical supply solutions reduce the risk of production downtimeLead Materials Scientist
Industry Overview
We do not just publish news; we construct a high-fidelity digital footprint for our partners. By aligning with TNE, enterprises build the essential algorithmic "Trust Signals" required by modern search engines, ensuring they stand out to high-net-worth buyers in an increasingly crowded global digital landscape.
Feed Delivery System Specifications Drive Cost Variability Beyond Base Price
Medium-scale poultry farms—typically operating 15,000 to 50,000 birds per cycle—face a recurring procurement challenge: equipment budgets often exceed initial quotes by 18–32% after final specification alignment. The feed delivery system accounts for 22–38% of total mechanization cost in such operations, yet its price sensitivity is rarely isolated in procurement workflows. Technical evaluators frequently treat it as a modular subsystem rather than a system-level cost driver—leading to late-stage budget revisions, installation delays, or compromised performance.
This cost volatility stems not from vendor markup but from how specifications interact across mechanical, electrical, environmental, and operational domains. A conveyor rated for 3.5 t/h may appear comparable on paper to one rated for 4.0 t/h—but the latter requires heavier-duty bearings, reinforced frame welds, upgraded motor windings, and recalibrated control logic. Each adjustment cascades into material selection, fabrication time, testing protocol, and warranty scope.
Material and Structural Specifications Define Long-Term Cost Trajectories
Stainless steel (304 vs. 316) choice affects more than corrosion resistance. In humid, high-ammonia barn environments, 316-grade components reduce maintenance frequency by 40–60% over five years—but increase upfront cost by 27–35%. However, that premium only pays off if the system operates >14 hours/day with minimal downtime. For farms running two-shift feeding cycles totaling <10 hours, 304 offers better lifecycle value.
Frame thickness matters beyond static load ratings. A 3-mm galvanized steel frame may meet ISO 50001 structural compliance, but under repeated vibration from auger-driven conveyors, fatigue cracks appear earlier in joints where stress concentration exceeds 120 MPa. Evaluators should request finite element analysis (FEA) reports—not just certification stamps—and verify mesh density used in simulation (≥15,000 elements recommended for dynamic loading models).
Control Architecture Determines Integration and Scalability Costs
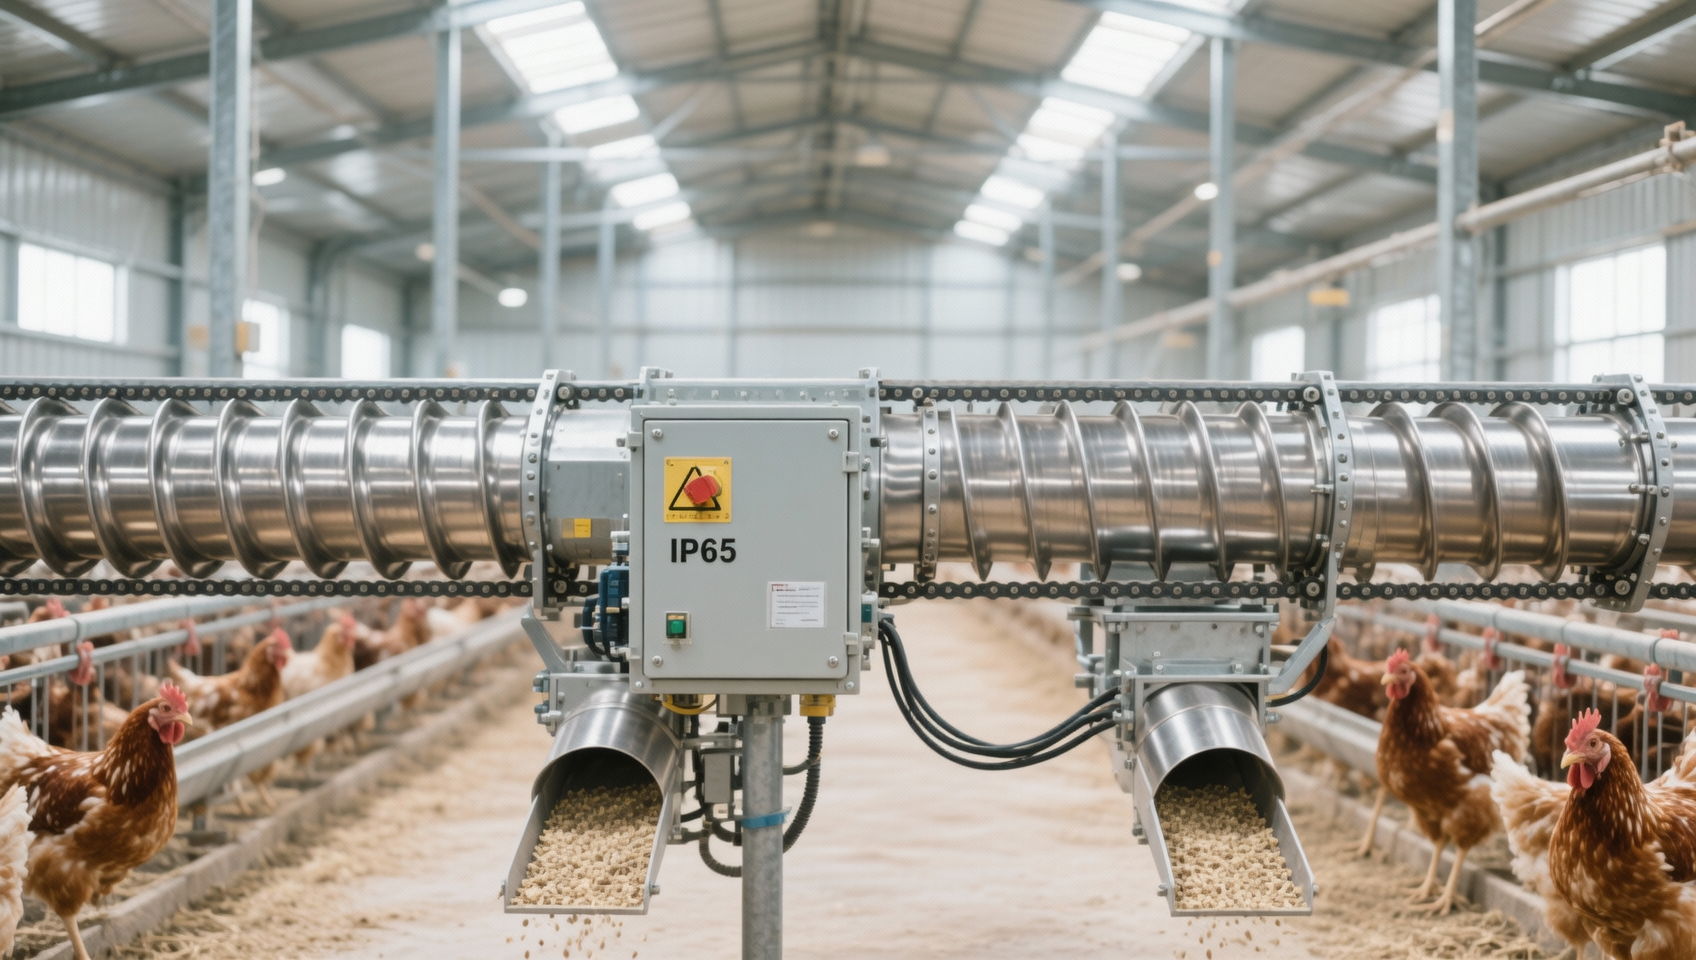
Basic systems use standalone PLCs with analog I/O and manual calibration dials. Advanced configurations integrate CAN bus communication, real-time feed mass monitoring via load cells, and API-based data export to farm management software. The difference isn’t just “smart vs. dumb”—it’s about integration labor. A CAN-enabled system may require no additional wiring for future flock tracking upgrades; an analog-only setup will need full rewiring and panel rework when adding IoT sensors.
Power supply design also impacts cost predictability. Systems specifying 24 VDC input only accept regulated power supplies—eliminating compatibility with standard 220 VAC farm distribution panels unless step-down transformers are added. That adds $320–$680 per unit, plus mounting space and thermal management considerations. Evaluators must cross-check voltage tolerance ranges against existing farm infrastructure—not just nameplate ratings.
Environmental Adaptation Adds Non-Linear Cost Layers
Dust ingress protection isn’t binary. IP54 prevents dust from interfering with operation—but doesn’t guarantee long-term seal integrity in high-humidity, condensation-prone environments. IP65-rated enclosures add 15–22% to electronics housing cost, but reduce sensor failure rates by 70% in tropical climates where daily dew point exceeds 22°C.
Similarly, temperature rating affects both component selection and thermal management. Motors rated for continuous operation at 55°C ambient require Class H insulation and forced-air cooling—costing 35–48% more than standard Class F units. Yet in naturally ventilated barns where summer roof temperatures reach 68°C, standard motors fail within 14 months. The decision hinges on actual measured barn microclimate—not regional weather averages.
Capacity and Throughput Parameters Alter Mechanical Load Profiles
Rated capacity assumes ideal conditions: uniform pellet size, 12% moisture content, and zero bridging. Real-world feed varies. When evaluating auger diameter and screw pitch, technical staff should test with local feed samples—not vendor-provided reference pellets. A 120 mm auger moving crumbled mash at 18% moisture may deliver only 65% of rated throughput, triggering cascading issues: longer cycle times, uneven distribution, and increased motor thermal cycling.
Belt-type conveyors introduce different variables. Belt width alone is insufficient. Tension retention capability—measured in N/mm² over 10,000 hours—determines whether tracking adjustments occur every 4 days or every 4 months. High-retention belts cost 2.3× more but cut labor hours by 68% annually in medium-scale operations where maintenance labor costs $24–$31/hour.
Delivery and Commissioning Requirements Influence Total Installed Cost
Pre-assembled skids reduce field labor but increase shipping weight and dimensional constraints. A fully assembled 18-meter feed line may exceed road transport limits in certain regions—requiring disassembly, custom crating, and reassembly fees averaging $1,200–$2,400. Modular systems avoid this but add 12–18 hours of on-site welding, alignment, and leak testing.
Commissioning scope directly affects handover timelines. Vendor-supplied commissioning typically covers functional verification only. Full validation—including feed distribution uniformity testing across all house zones, calibration traceability to NIST standards, and documentation of torque values applied to critical fasteners—adds 9–14% to base equipment cost but reduces first-year operational variance by up to 44%.
Where Specifications Meet Procurement Reality
Technical evaluators often overlook how specification granularity affects supplier response quality. A tender asking for “stainless steel construction” yields inconsistent interpretations—some quoting 304 sheet metal with carbon steel supports, others using full 316 assemblies. Requiring ASTM A240/SA240 grade callouts, minimum tensile strength (≥515 MPa), and grain size reporting (ASTM E112) produces comparable bids.
This precision enables meaningful comparison. Without it, price lists become misleading artifacts—not decision tools. A poultry farm equipment price list that groups systems solely by capacity or brand fails to reflect these specification-driven cost deltas. Effective evaluation demands side-by-side parameter mapping: motor insulation class, belt splice method, enclosure IP rating, and control loop update frequency—not just headline pricing.
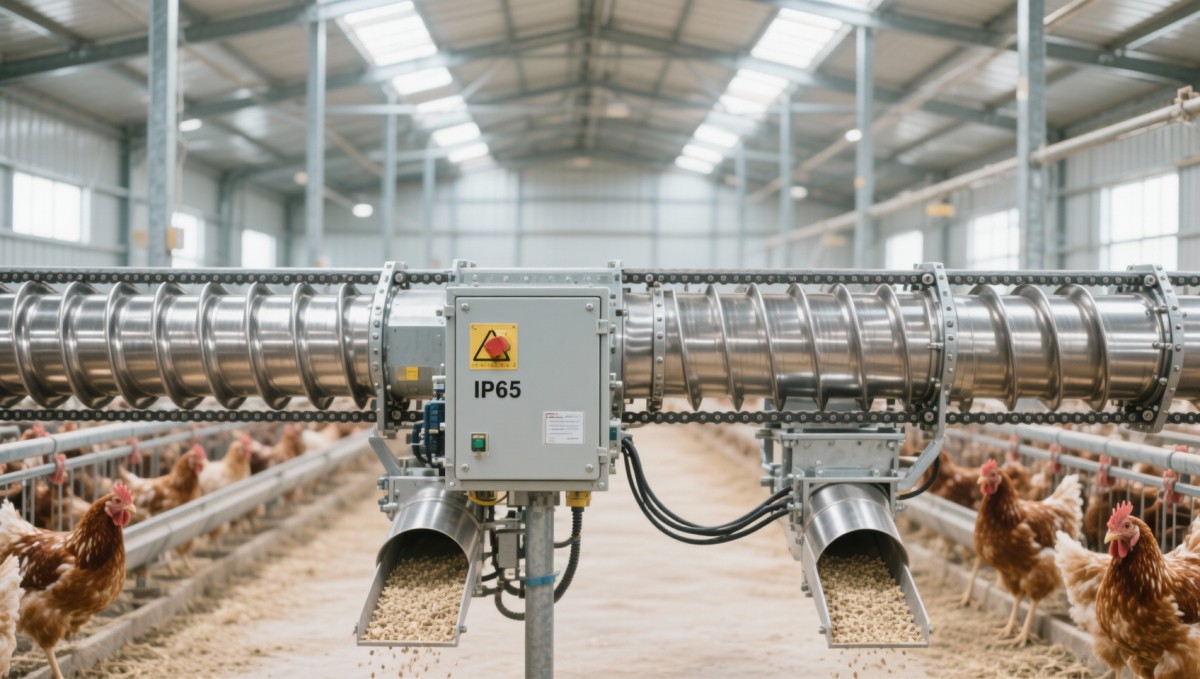
For medium-scale farms, the feed delivery system isn’t a commodity purchase. It’s a system whose specifications define mechanical longevity, energy consumption, labor dependency, and data fidelity. Treating it as such avoids cost surprises—and ensures capital investment aligns with operational reality.
Next:No more content
Deep Dive
Related Intelligence
 Livestock & Poultry TechChina's Export of Veterinary Antibiotics Surges 18.7% YoY in Q1 2026: Key Industry Impacts and ResponsesAnalyst:Agri-Tech Strategist
 Livestock & Poultry TechChina Feed Industry Association Initiates Revision of Microbial Fermented Feed Additives Group StandardAnalyst:Agri-Tech Strategist
 Livestock & Poultry TechNational Feed Quality Inspection Center Releases Q1 2026 Feed Safety Report: Key Impacts and Industry ResponsesAnalyst:Agri-Tech Strategist